Advanced IC Reactor for Fermentation Wastewater Treatment: A Complete Guide to High-Efficiency Anaerobic Digestion
In recent years, the industrial fermentation sector has experienced exponential growth across pharmaceuticals, alcohol production, biofuels, enzymes, and food additives. This expansion brings a pressing need to manage fermentation wastewater, which is characterized by high concentrations of organic matter, volatile fatty acids, and complex nutrients . As industries seek sustainable and cost-effective treatment options, Internal Circulation (IC) Reactors have emerged as one of the most efficient anaerobic treatment technologies available.
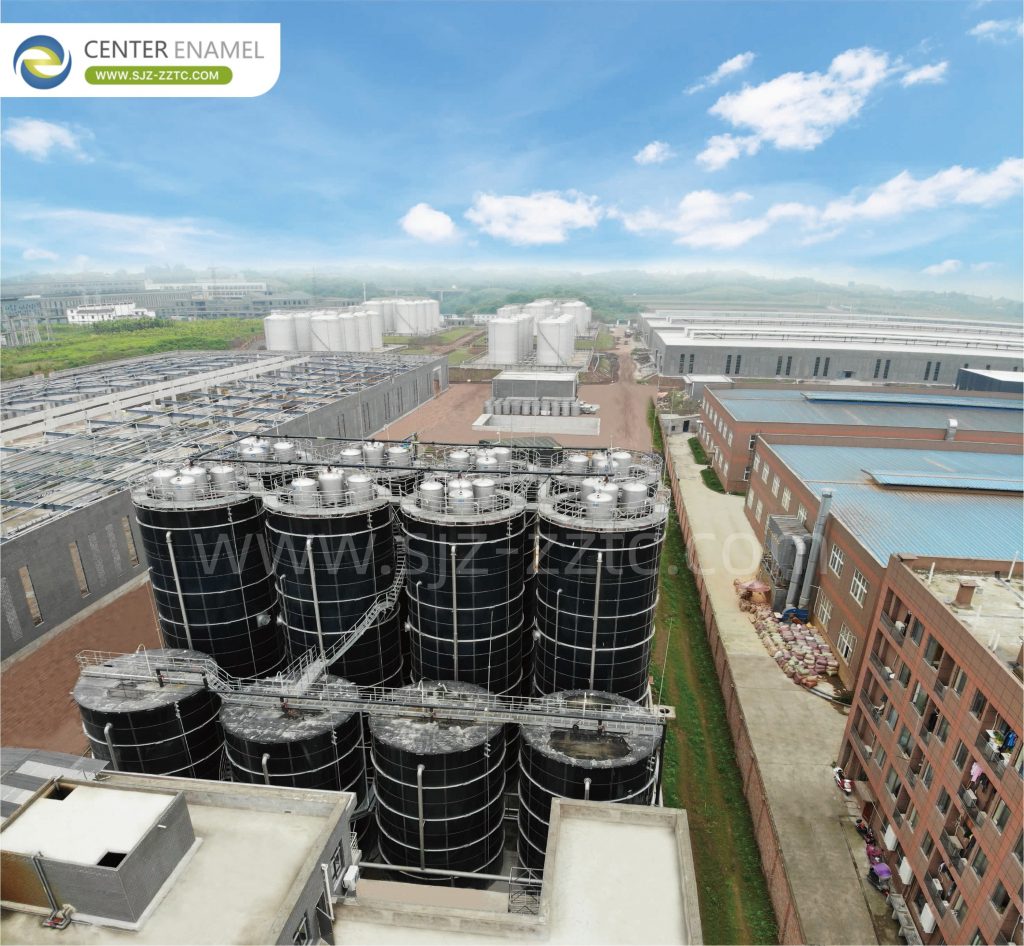
The IC reactor represents the third generation of anaerobic technology for high-strength industrial wastewater treatment, increasingly displacing traditional Upflow Anaerobic Sludge Blanket (UASB) processes and other conventional anaerobic treatment methods . When developed and implemented by a trusted IC reactor manufacturer such as Shijiazhuang Zhengzhong Technology Co., Ltd. (Center Enamel), these systems become reliable, long-lasting assets for wastewater management.
With more than 30 years of experience in design and manufacture of high-performance anaerobic digestion systems, Center Enamel has become a global leader in wastewater treatment solutions, delivering turnkey projects in over 90 countries across six continents .
Project Overview: Fermentation Wastewater Treatment with IC Reactor Technology
Project Background
Fermentation wastewater presents unique treatment challenges due to its high organic loading, variable composition, and presence of complex compounds. Industries such as pharmaceutical production, amino acid manufacturing, and biofuel production generate effluents that require robust, high-performance treatment solutions . Traditional aerobic treatment methods demand significant energy input and produce large quantities of biomass requiring disposal .
The IC reactor addresses these challenges through its innovative two-stage anaerobic design, offering high organic load capacity, compact footprint, and valuable biogas recovery .
Scope of Work
A comprehensive fermentation wastewater treatment project utilizing IC reactor technology encompasses:
Pre-treatment: Equalization, pH adjustment, and nutrient balancing
Anaerobic Digestion: IC reactor for high-rate COD removal and biogas generation
Biogas Management: Collection, purification, and energy recovery systems
Post-treatment: Optional aerobic polishing for ultra-low discharge limits
Sludge Management: Dewatering and beneficial reuse of digested solids
Key Technologies Used
| Technology Component | Description | Function |
| Internal Circulation (IC) Reactor | Two-stage anaerobic reactor with internal recirculation | High-rate COD removal with biogas generation |
| Fusion-Bonded Epoxy (FBE) Coated Tanks | Bolted steel tanks with electrostatic powder coating | Superior corrosion resistance against H₂S and organic acids |
| Double Membrane Gas Storage | Dual-layer roof system for biogas capture | Safe gas collection with pressure regulation |
| SCADA Automation | Real-time monitoring and control system | Process stability optimization |
| Aluminum Dome Roofs | Corrosion-resistant geodesic structures | Odor control and rainwater exclusion |
Why IC Reactors Are Ideal for Fermentation Wastewater Treatment
IC Reactors have revolutionized anaerobic treatment by offering enhanced bioconversion rates, compact design, and high energy recovery through biogas generation. Their structural and operational advantages make them uniquely suited for fermentation wastewater, which includes a mix of sugars, ethanol residues, yeast by-products, and nutrient-rich effluents .
High Organic Load Capacity
IC reactors can treat wastewater with relatively high COD concentrations, making them ideal for fermentation-based industries such as breweries, distilleries, and amino acid production plants . Research has demonstrated successful IC reactor application for pharmaceutical-grade lactose wastewater with high organic content .
Two-Stage Anaerobic Digestion
The IC reactor's vertical structure accommodates two anaerobic digestion stages. In the lower reactor zone, active sludge is maintained for hydrolysis and acidogenesis. In the upper stage, methane production occurs, resulting in higher biogas output and more stable effluent quality . This configuration, based on two UASB reactors connected in series, offers excellent operational stability and COD removal even at high organic loading rates .
Efficient Sludge Management
IC reactors produce significantly lower sludge volumes due to optimized microbial retention and internal circulation, minimizing sludge disposal costs and environmental impact. Anaerobic treatment typically results in less biomass production compared to aerobic processes .
Rapid Start-Up and Recovery
The reactor's structure supports fast accumulation of biomass, reducing start-up time to just a few weeks. In the event of shock loading or system interruption, recovery is quicker than with conventional reactors . Proper start-up protocol using granular seed sludge and gradual loading increases is essential for establishing stable granular sludge bed formation .
Biogas Utilization
The high biogas production from fermentation wastewater can be collected and reused as fuel for Combined Heat and Power (CHP) systems, offsetting energy costs and contributing to a circular economy. For high-strength industrial wastewater treatment, biogas yield represents approximately 0.35 m³ biogas per kg COD removed .
Reduced Odor and Greenhouse Gas Emissions
With sealed construction and efficient gas collection systems, IC reactors minimize odor emissions and greenhouse gases, improving workplace conditions and sustainability compliance .
Industry Applications and Global Project Implementation
Center Enamel's IC reactor systems have been successfully deployed in fermentation plants worldwide, addressing diverse wastewater characteristics and treatment objectives .
1. Pharmaceutical Fermentation Plants
Pharmaceutical production, especially antibiotics and enzymes, generates highly variable wastewater with complex chemical structures. IC reactors, with their robust microbial communities and internal mixing design, adapt effectively to these fluctuations .
Case Example: Center Enamel's modular IC reactor units in India treat effluent from penicillin and streptomycin production. Research on pharmaceutical-grade lactose wastewater demonstrates that IC reactors successfully handle high-COD streams that previously required energy-intensive evaporation and drying processes .
2. Amino Acid and Organic Acid Production
Industries producing lysine, glutamic acid, or citric acid release wastewater with high organic acid loads and low pH. IC reactors accommodate this through pre-neutralization and tailored biomass retention strategies . Center Enamel has designed systems in China and South Korea specifically for such applications, achieving high treatment efficiency and process stability.
3. Biofuel and Bioplastics Fermentation
Wastewater from ethanol and bioplastic production contains volatile fatty acids, glycerol, and by-products of fermentation—excellent substrates for anaerobic digestion. IC reactors by Center Enamel have been implemented in bioethanol plants to reduce treatment costs and increase energy self-sufficiency through methane recovery .
4. Brewery and Distillery Applications
The IC reactor has been successfully used for brewery wastewater treatment, with full-scale systems demonstrating stable performance over extended operation periods . Design considerations for such applications include hop acid acclimation, ethanol inhibition management, and nutrient balance optimization .
Technical Design and Operational Considerations
Critical Process Constraints
Successful IC reactor implementation requires addressing specific challenges common in fermentation wastewater:
| Challenge | Impact | Mitigation Strategy |
| Ethanol Inhibition | Concentrations >2,000 mg/L inhibit acetoclastic methanogens | Equalization and dilution blending |
| pH Fluctuations | VFA accumulation can cause pH crash | Maintain 2,000–4,000 mg/L CaCO₃ alkalinity |
| Nutrient Deficiency | Many fermentation wastewaters lack N and P | Target COD:N:P ratio of 350:5:1 |
| Sulfide Toxicity | Dissolved H₂S >150 mg/L is toxic to methanogens | Iron chloride dosing or micro-aeration |
Temperature Control and Stability
Temperature plays a critical role in anaerobic digestion performance. Mesophilic operation (35 ± 2°C) is standard for most fermentation applications, with insulated vessels reducing heat loss by 60–70% . Thermophilic operation (55°C) offers faster reaction rates but requires careful management of ammonia inhibition risks .
Monitoring and Control
Comprehensive monitoring ensures stable IC reactor performance:
Online pH monitoring with automatic alarms
Volatile fatty acid analysis (VFA:alkalinity ratio as primary stability indicator)
Gas flow and composition monitoring (methane percentage drop warns of organic overload)
Daily COD measurement to track loading rates
Fusion-Bonded Epoxy Tank Technology: The Foundation of Reliable IC Reactors
The combination of IC reactors with fusion-bonded epoxy (FBE) coated steel tanks offers unmatched durability and process stability for fermentation wastewater treatment .
Superior Resistance to H₂S Corrosion
Anaerobic digestion generates hydrogen sulfide (H₂S) that, when combined with moisture, forms sulfuric acid—a primary cause of structural failure in unprotected digesters. The FBE coating provides a dense, high-performance thermoset polymer barrier molecularly bonded to steel, offering long-term protection against corrosive attack .
Guaranteed Gas-Tight Design
The modular, bolted structure utilizes precision-engineered panels and advanced sealants to ensure a perfect seal at every seam, making the tank gas-tight under pressure. This integrity is fundamental to safety, compliance, and maximizing biogas collection efficiency .
Chemical Resistance and Durability
FBE coatings resist corrosion from volatile fatty acids and cleaning agents commonly found in fermentation effluents. Smooth epoxy surfaces prevent scaling and biofilm formation, ensuring consistent reactor performance with minimal maintenance .
Modularity and Scalability
Systems can be easily upgraded or relocated, making them ideal for growing fermentation plants or multi-site operations. Tank capacities range from 20 m³ to 18,000 m³ .
Comparative Advantages
Performance data indicates that fusion-bonded epoxy coating offers advantages over traditional glass-lined tanks in bolted construction, including superior strength, repairability in the field, and cost-effectiveness .
Project Results and Performance Data
| Parameter | Performance Range | Notes |
| COD Removal Efficiency | 60–80%+ | Dependent on wastewater characteristics and operating conditions |
| Biogas Yield | 0.35 m³ per kg COD removed | Approximate theoretical yield |
| Energy Recovery | ~1.47 kWh per kg COD removed | Net energy balance from CHP |
| Start-Up Period | 3–6 months to full load | With proper granular seed sludge |
| HRT Range | Varies by application | Designed for high-rate treatment |
| Sludge Reduction | 70–90% less than aerobic | Compared to conventional aerobic treatment |
Considerations for Selecting an IC Reactor Manufacturer
When planning a fermentation wastewater treatment project, choosing the right IC reactor manufacturer is critical to project success. Center Enamel distinguishes itself through the following key strengths:
1. Custom Design Expertise
Each IC reactor is customized based on wastewater characteristics, treatment objectives, and site limitations. Center Enamel employs advanced modeling software and laboratory-scale trials to ensure optimal reactor sizing and performance .
2. Material Innovation: Fusion-Bonded Epoxy Tanks
Center Enamel's reactors are paired with FBE coated steel tanks offering superior resistance to corrosion, pH fluctuations, and high internal pressures. Their bolted modular design enables faster installation and easy future expansion .
3. Integrated Engineering and Automation
The company provides complete systems including feeding systems, gas holders, mixing units, sludge handling, and SCADA automation. Real-time monitoring ensures stable performance even under variable loading .
4. Global Project Implementation
Center Enamel's IC reactor systems have been successfully deployed in more than 100 countries, spanning Africa, Southeast Asia, Europe, and Latin America with experience across cultures, regulations, and climate conditions .
5. Certifications and Compliance
All systems conform to international standards including ISO9001, ISO14001, ISO45001, and NSF/ANSI 61 for tank coatings .
Client Testimonials
"Center Enamel's IC reactor solution transformed our pharmaceutical fermentation wastewater treatment. The system handles our variable COD loads reliably and the biogas generated now offsets a significant portion of our facility's energy costs."
"The fusion-bonded epoxy tank construction has proven exceptionally durable in our bioethanol plant. After three years of continuous operation, the tank shows no signs of corrosion despite the aggressive wastewater chemistry."
Future Trends and Sustainable Impact
As fermentation industries move toward green production and net-zero goals, IC reactors offer an ideal solution for waste-to-energy conversion, water recycling, and carbon footprint reduction. Center Enamel continues to invest in R&D to optimize reactor designs for higher loading rates, lower energy input, and improved nutrient recovery .
Emerging trends include:
AI-Powered Process Optimization: Machine learning algorithms being incorporated into control systems to predict reactor performance and optimize feed dosing .
Integration with Aerobic Polishing: IC reactors followed by MBR or SBR units to meet ultra-low discharge limits.
Nutrient Recovery Systems: Technologies being developed to recover nitrogen and phosphorus from fermentation wastewater for reuse in agriculture or industry.
Conclusion
Center Enamel's advanced IC reactor systems offer a powerful solution for fermentation wastewater treatment, optimizing organic removal efficiency, enabling biogas generation, and supporting sustainable water management. With advantages including high organic load capacity, compact design, reduced sludge production, and rapid start-up, IC reactors are essential for achieving long-term success in fermentation industry wastewater management.
As global demands for sustainable industrial practices intensify, the integration of advanced anaerobic digestion technologies—supported by robust infrastructure like FBE tanks and comprehensive gas management systems—will continue to drive the transition from waste disposal to resource recovery .
Frequently Asked Questions (FAQ)
What is an Internal Circulation (IC) reactor?
The IC reactor is a third-generation anaerobic technology based on two UASB reactors connected in series, featuring a tall vertical structure with internal recirculation that enhances contact between wastewater and active biomass. It is particularly effective for high-strength industrial wastewater treatment .
What types of fermentation wastewater can IC reactors treat?
IC reactors are suitable for diverse fermentation wastewater streams including pharmaceutical production (antibiotics, enzymes), amino acid manufacturing, biofuel production, brewery and distillery effluents, and food additive processing .
What are the advantages of IC reactors over traditional UASB systems?
IC reactors offer excellent operational stability, high COD removal even at elevated organic loading rates, a compact footprint (taller design with high height-diameter ratio), and faster start-up compared to UASB systems that typically require 2–8 months for granular sludge formation .