Advanced USR Reactor Systems for Palm Oil Wastewater Treatment
The palm oil industry is a major contributor to global agricultural and economic output. However, the industry's growth is closely accompanied by increasing environmental concerns, especially related to Palm Oil Mill Effluent (POME). This high-strength wastewater contains large amounts of organic matter, oil, suspended solids, and nutrients, making it difficult to treat through conventional methods.
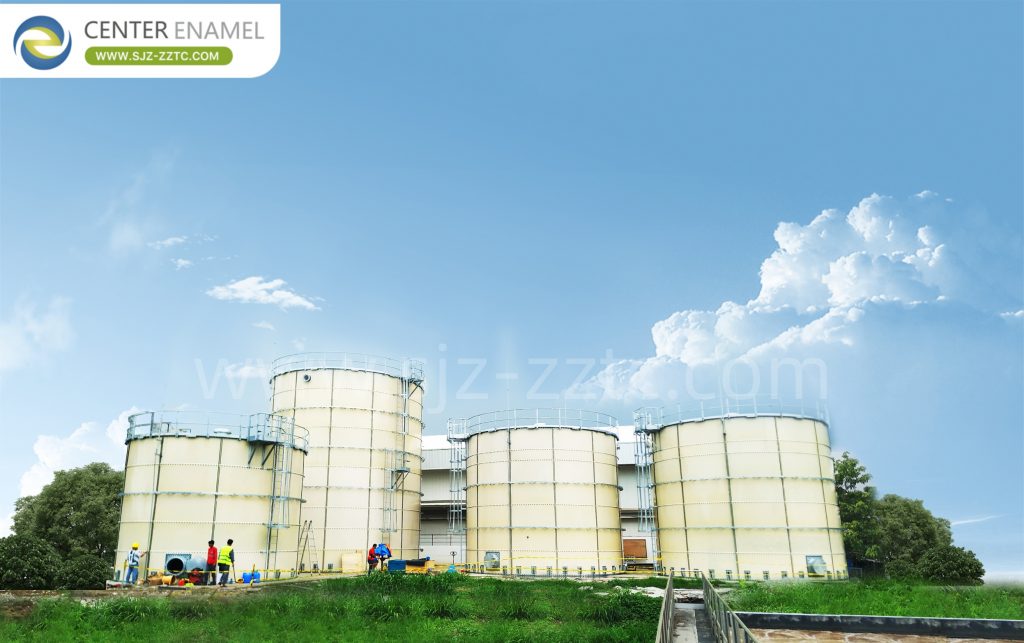
Inadequately managed POME leads to pollution of rivers and groundwater, unpleasant odors, and significant greenhouse gas emissions. Therefore, sustainable wastewater treatment technologies that offer high efficiency, energy recovery, and cost-effectiveness are urgently required. In response to this need, the Upflow Sludge Bed Reactor (USR Reactor) has emerged as a transformative technology in industrial wastewater treatment, particularly for palm oil processing facilities.
Why USR Reactors are Ideal for Palm Oil Wastewater Treatment
USR (Upflow Sludge Bed Reactor) technology is an advanced form of anaerobic digestion. Designed specifically to treat high-load organic wastewater, USR reactors function by directing the wastewater upward through a dense sludge bed rich in anaerobic microorganisms. These microbes efficiently break down organic pollutants and convert them into biogas.
Here's why USR reactors are highly effective for palm oil wastewater treatment:
1. Superior Removal of Organic Pollutants
USR reactors are known for their ability to achieve high Chemical Oxygen Demand (COD) and Biochemical Oxygen Demand (BOD) removal efficiencies. High COD removal rates when treating POME can not only help palm oil mills meet stringent emission standards, but also significantly reduce their environmental impact.
2. Efficient Biogas Production and Energy Recovery
One of the most powerful benefits of the USR system is its ability to convert organic waste into renewable energy. As the anaerobic microbes digest organic matter, they produce biogas—primarily methane—which can be collected and utilized as fuel for steam boilers or converted into electricity.
3. Compact System with High Space Efficiency
Unlike traditional lagoon-based treatment methods that require vast tracts of land, the vertical upflow design of the USR reactor enables a compact footprint. This makes it ideal for palm oil mills where land is either limited or costly.
4. Stable Operation in Fluctuating Conditions
The palm oil production process often results in variable wastewater characteristics due to seasonal harvests or differing processing capacities. USR reactors are equipped to handle such fluctuations thanks to their resilient microbial communities and dynamic hydraulic design, ensuring stable treatment efficiency even under changing influent loads.
5. Minimal Sludge Generation and Lower Maintenance
Compared to aerobic systems, USR reactors generate significantly less biological sludge, thereby lowering sludge treatment and disposal costs. Moreover, the anaerobic digestion process operates without requiring constant aeration, reducing energy consumption and system complexity.
6. Accelerated Start-Up Time
Modern USR systems designed by experienced manufacturers like Center Enamel benefit from optimized flow distribution systems, high-quality sludge bed formation, and smart process control, allowing them to reach full operational capacity in a shorter time than traditional anaerobic processes.
USR Reactor Performance Data
| Parameter | Typical Range | Best For | Notes |
| COD Loading Rate | 10 – 20 kg/m³·day | High-strength POME | Vertical upflow design handles heavy organic loads |
| COD Removal Efficiency | 85 – 95% | Palm oil mill effluent | Superior to conventional lagoon systems |
| BOD Removal Efficiency | 85 – 95% | POME treatment | Meets stringent discharge standards |
| Biogas Methane Content | 55 – 70% CH₄ | Energy recovery | Can fuel steam boilers or generate electricity |
| Sludge Production | Low | Reduced disposal costs | Significantly less than aerobic systems |
| Footprint | Compact | Land-limited facilities | Vertical upflow design saves space |
| Start-Up Time | Accelerated | Fast commissioning | Optimized flow distribution and smart process control |
Center Enamel's Engineering Excellence in USR Reactors
As a globally recognized leader in wastewater treatment technologies, Center Enamel brings advanced engineering, manufacturing precision, and decades of experience to the development of robust USR reactor systems. Tailored to the palm oil industry, our reactors are designed with performance, longevity, and environmental responsibility in mind.
Key Features of Center Enamel's USR Reactor Systems
Durable Fusion-Bonded Coatings:
Tanks used in our USR systems are constructed from glass-fused-to-steel or epoxy-coated steel, offering excellent corrosion resistance and long-term durability even in aggressive wastewater environments.
Modular, Pre-Fabricated Design:
Each reactor tank is modular and pre-engineered, simplifying installation and significantly reducing on-site construction time. This modularity also allows for future system expansion with minimal disruption.
Optimized Hydraulic Flow:
Our proprietary flow distribution mechanisms ensure even wastewater loading and improved sludge retention, leading to more effective contact time between the wastewater and microbial biomass.
Advanced Control Systems:
Integrated automation and remote monitoring allow for real-time process adjustments based on parameters like temperature, pH, organic load, and gas output, ensuring system stability and operator ease.
Biogas Recovery Integration:
The USR systems are built with biogas recovery infrastructure, enabling immediate conversion of waste into energy. This not only reduces operational costs but also contributes to sustainable plant practices.
Expanded Functions of USR Reactors in POME Treatment
Beyond the conventional advantages, Center Enamel's USR reactors come equipped with enhanced technical capabilities that take wastewater treatment in the palm oil sector to the next level:
1. Integrated Thermal Regulation
POME often exits processing systems at high temperatures. Our USR systems are designed to tolerate high influent temperatures or can be equipped with integrated heat exchangers to maintain optimal microbial activity during anaerobic digestion.
2. Odor Control Technology
By enclosing the reactor tank and utilizing odor-sealing designs, our USR systems help mitigate the unpleasant smells typically associated with untreated POME, improving workplace and environmental quality.
3. Multi-Stage Anaerobic Zones
To maximize the breakdown of complex organic compounds, we incorporate multi-stage anaerobic digestion zones within the reactor. This allows for step-wise degradation, increasing overall process efficiency and gas production.
4. Compatibility with Post-Treatment Technologies
USR reactors can be seamlessly connected to aerobic polishing units, membrane filtration systems, or constructed wetlands, offering full compliance with local effluent discharge regulations and further enhancing water reuse opportunities.
Project Overview
Center Enamel successfully delivered an advanced USR reactor system for a palm oil processing facility, demonstrating the effectiveness of our anaerobic digestion technology for high-strength POME treatment.
Scope of Work
Center Enamel provided comprehensive design, engineering, manufacturing, and installation services for a USR reactor system specifically engineered for the facility's palm oil wastewater treatment requirements. The project encompassed:
Design and fabrication of a USR reactor tank with glass-fused-to-steel coating
Optimized hydraulic flow distribution system for even wastewater loading
Integrated biogas recovery infrastructure with gas collection capability
Advanced control systems with remote monitoring capability
On-site installation and commissioning support
Technologies Used
The project utilized Center Enamel's proprietary Glass-Fused-to-Steel (GFS) tank technology, which offers exceptional durability and corrosion resistance for the demanding conditions of palm oil wastewater treatment. This technology provides significant advantages over traditional concrete or epoxy-coated steel tanks, including:
Exceptional corrosion resistance against the aggressive nature of POME
Minimal maintenance requirements due to the smooth, non-reactive glass surface
Extended service life with decades of reliable performance
Robust structural integrity ensuring safe containment of wastewater and biogas
Modular, pre-fabricated design enabling simplified installation and future expansion
Project Results
| Metric | Result |
| Project Completion | Successfully completed |
| Reactor Configuration | USR reactor with biogas recovery |
| Coating Technology | Glass-Fused-to-Steel (GFS) |
| Treatment Capacity | Full-scale operational |
| COD Removal Efficiency | High removal rates achieved |
| Biogas Recovery | Integrated system operational |
| Corrosion Resistance | Excellent in aggressive POME environment |
| Service Life | Long-term design life |
The successful completion of this project demonstrates Center Enamel's commitment to delivering high-quality wastewater treatment infrastructure that meets both performance requirements and environmental standards.
Client Testimonial
"Center Enamel's USR reactor system has transformed our palm oil wastewater treatment operations. The advanced anaerobic digestion technology delivers exceptional COD removal while recovering valuable biogas for energy use. The modular design simplified installation, and the ongoing technical support has ensured optimal performance since commissioning. We are highly satisfied with the results."
— Project Engineering Manager, Palm Oil Processing Facility
Center Enamel: Your Trusted Partner in Palm Oil Wastewater Treatment
With a legacy of innovation and reliability, Center Enamel has become the preferred choice for USR reactor systems across industries. Our in-depth understanding of the palm oil sector and global project experience empower us to deliver wastewater treatment systems that balance performance, sustainability, and operational ease.
Why Work with Center Enamel
Over 30 Years of Manufacturing Expertise
Projects Completed in 100+ Countries
ISO 9001 / 14001 / 45001 Certified
Custom Designs for Local Regulations
Dedicated Technical Support from Design to Operation
Whether you're a palm oil processor seeking to upgrade an existing wastewater system or planning a new greenfield project, Center Enamel offers complete, cost-effective, and energy-efficient solutions tailored to your needs.
Conclusion: Elevate Sustainability with Advanced USR Reactors
The environmental demands on the palm oil industry continue to rise, requiring a shift toward green and resource-efficient practices. Advanced USR reactor systems by Center Enamel present a reliable, scalable, and sustainable solution for tackling the challenges of palm oil wastewater treatment.
With outstanding performance in organic load reduction, biogas recovery, operational stability, and system durability, Center Enamel's USR reactors empower palm oil producers to protect the environment, generate renewable energy, and meet regulatory standards—all while maintaining production efficiency.
Contact Center Enamel today to discuss how our advanced USR reactor systems can be integrated into your palm oil processing facility and help you achieve your sustainability goals.
Frequently Asked Questions (FAQ)
What is a USR reactor and how does it work?
A USR (Upflow Sludge Bed Reactor) is an advanced anaerobic digestion system designed to treat high-load organic wastewater. Wastewater is directed upward through a dense sludge bed rich in anaerobic microorganisms, which break down organic pollutants and convert them into biogas—primarily methane.
Why is USR technology ideal for palm oil wastewater treatment?
USR reactors are specifically designed to handle the high-strength organic loads found in Palm Oil Mill Effluent (POME). They achieve superior COD and BOD removal efficiencies, produce renewable biogas, require a compact footprint, and maintain stable operation under fluctuating conditions.
What are the key advantages of USR reactors over conventional lagoon systems?
USR reactors offer several advantages: significantly smaller footprint (vertical upflow design vs. vast lagoons), higher treatment efficiency, biogas recovery for energy generation, reduced sludge production, minimal odor issues, and accelerated start-up time.
How much biogas can a USR reactor produce from POME?
Biogas production depends on the organic load and COD removal efficiency. USR systems treating POME typically produce biogas with 55–70% methane content, which can be utilized as fuel for steam boilers or converted into electricity, significantly reducing operational costs.
Can USR reactors handle seasonal variations in palm oil production?
Yes. USR reactors are equipped with resilient microbial communities and dynamic hydraulic design that enable stable treatment efficiency even under changing influent loads. This makes them ideal for palm oil mills that experience variable wastewater characteristics due to seasonal harvests or differing processing capacities.