
Integrated Biogas Plant Design with USR Process for POME Treatment Applications
The competitive landscape shows divergence, with leading companies building integrated service capabilities through technical integration and capital operations, and industry concentration gradually increasing. Chinese companies continue to consolidate their advantages in mid-tier equipment exports. International giants target high-end customers and complex industrial wastewater markets, while local players occupy the mid- to low-end and industrial park centralized treatment markets with service responsiveness and cost advantages.
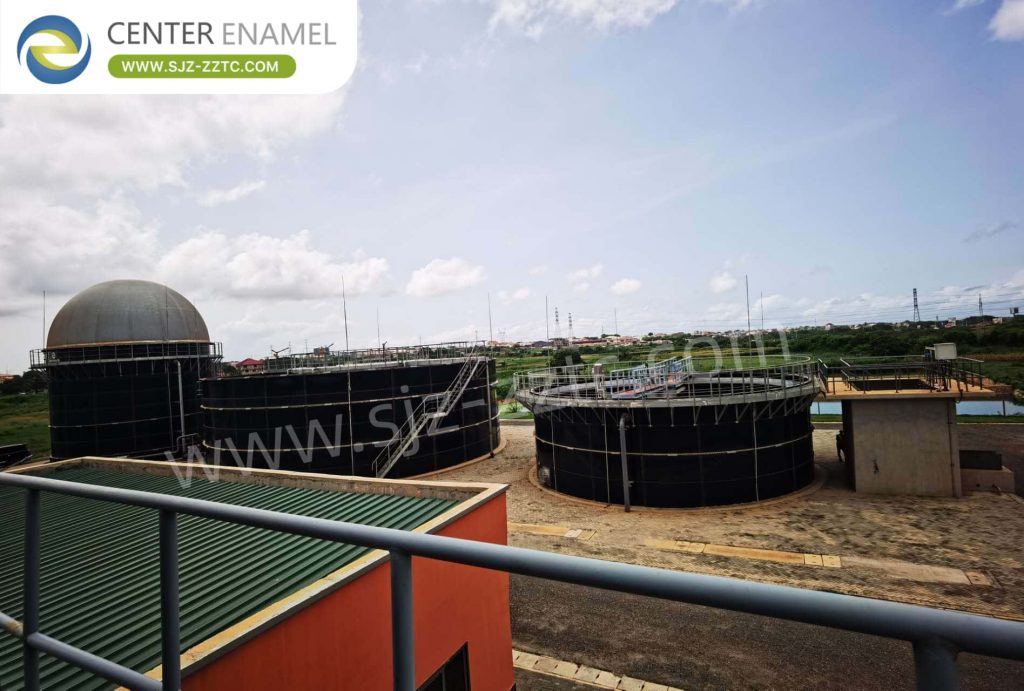
In the anaerobic process segment, UASB, EGSB, and IC anaerobic reactors, with advantages of high loading rates, small footprints, and stable operation, are widely used in high-concentration organic wastewater pretreatment in food processing, pharmaceutical fermentation, alcohol brewing, chemical, and other industries. These reactors use steel tank shells, and their corrosion resistance and gas-tightness directly determine long-term operational stability. The application value of glass-fused-to-steel tanks in such scenarios is increasingly prominent. This trend toward integrated, durable infrastructure is especially relevant for POME Treatment, where aggressive wastewater characteristics demand both robust process design and corrosion-resistant tank construction. Proper Biogas Plant Design must therefore account for tank integrity as a core element of long-term operational success.
USR Process Reaction Mechanism for High-Solids Organic Wastewater
High-solids organic wastewater, after simple pretreatment to remove large debris, is uniformly fed into the reactor through the bottom distribution system. The upward flow drives solid substrates and anaerobic sludge to slowly rise and thoroughly mix. In the sealed anaerobic environment, microorganisms sequentially hydrolyze/acidify and then methanogenically ferment, degrading macromolecular organic pollutants and generating biogas and treated water. Without complex separation structures, gentle hydraulic disturbance prevents clogging.
The mixed liquor rises to the upper portion of the reactor where natural gas-liquid-solid separation occurs. Biogas is collected, effluent overflows, and solid sludge and unreacted substrate settle back to the lower reaction zone for continued reaction, with a small amount of aged sludge periodically discharged-continuous stable operation. This simple yet effective mechanism makes the USR Process particularly well-suited for challenging waste streams, and it forms the biological core of any well-engineered Biogas Plant Design targeting high-solids wastewater. When applied to POME Treatment, the USR Process delivers reliable performance where conventional anaerobic systems frequently fail.
Palm Oil Mill Effluent Key Water Quality Characteristics
Palm oil mill effluent (POME) presents a prominent “five highs and one low” profile-high COD, high BOD, high oil and grease, high suspended solids, high temperature, low pH-pollution load far exceeding conventional industrial wastewater, one of the highest concentration wastewater categories in agricultural processing. Very high COD-combined wastewater 45,000–100,000 mg/L, oil separation wastewater peaking above 150,000 mg/L-dozens to hundreds of times higher than municipal wastewater.
High BOD-25,000–65,000 mg/L, BOD/COD 0.5–0.6-excellent biodegradability with very high anaerobic digestion efficiency. High oil and grease-combined 2,000–8,000 mg/L, oil separation above 10,000 mg/L-oil readily adheres and scales on pipe/equipment surfaces, affecting heat transfer and causing blockages. High suspended solids-10,000–20,000 mg/L-primarily fruit pulp residues, fruit shell fibers, colloidal proteins-readily settling and clogging equipment. Moderate total nitrogen-ammonia 500–1,500 mg/L with abundant organic nitrogen but low inorganic nitrogen.
High total phosphorus-200–800 mg/L. Very low pH-raw water pH 4.0–5.0-requires alkali neutralization before biological treatment. High temperature-discharge 60–80°C-requires cooling to 35–38°C before anaerobic digestion. Water quality varies significantly with palm oil mill processing seasons-peak production during fresh fruit bunch harvest season (March–September annually) with full-load operation, wastewater volume and organic concentration at maximum; off-season (October–February) with reduced or halted production-water quality fluctuations require high shock load resistance. These extreme characteristics directly dictate the technical requirements for effective POME Treatment and demand a Biogas Plant Design that integrates high-solids tolerance, oil management, and temperature control from the outset.
Center Enamel’s Smart Manufacturing Base Scale and Capability
Center Enamel‘s core intelligent manufacturing base is located in Hebei Province, China, covering a total area of over 150,000 m², with Phase I mature manufacturing facility and Phase II high-end environmental equipment industrial park-dual-base synergy ensures stable production capacity. The base includes dedicated R&D office buildings, proprietary material laboratories, and finished product testing centers, with full-process quality control systems meeting ISO, NSF, CE, and other international standards. The facility operates to green manufacturing standards, certified as a Provincial Green Factory-balancing efficient production with energy conservation and emission reduction.
The company has 6 marketing service centers across China, establishing a nationwide production-sales network ensuring stable global order delivery. The base is adjacent to expressway networks and major logistics hubs, with complete container shipping capabilities-supporting simultaneous large-scale tank projects globally. The base employs over 500 staff, with multiple parallel automated production lines-facility scale and production capacity firmly placing it among the global top tier of GFS tank equipment manufacturers. This manufacturing strength provides the physical foundation for delivering every Biogas Plant Design and USR Process system on time and to specification, regardless of project scale or location.
Over a Decade of Global Installation Experience
Unmatched global practical experience among domestic peers-over a decade covering multiple regions and all industry sectors. In 2009, Center Enamel completed the first overseas GFS tank installation-sending a team to Niger, Africa for drinking water storage tank installation. In 2015, it broke industry ground with China’s first GFS tank export and installation to the US-passing strict US acceptance standards. All installed projects have operated stably for many years, demonstrating the durability and reliability that underpin every Biogas Plant Design and POME Treatment system the company delivers. This accumulated field experience directly informs the engineering decisions behind each new USR Process installation.
Center Enamel Design Team and Customized Engineering Capability
The design team includes senior engineers registered in the Hebei Provincial Science and Technology Expert Database, with design standards aligned with strict European/American high-end equipment safety standards. The team can provide complete integrated design for differentiated overseas projects in livestock biogas, POME, municipal wastewater, hazardous waste storage, seawater desalination, etc.-covering tank structure, anti-corrosion/sealing systems, biogas piping, and anaerobic process integration.
Pre-design thoroughly investigates local seismic zone, wind pressure, soil bearing capacity, water quality corrosivity, and local environmental discharge standards-applying thickened panels, reinforced anchored bases, and optimized sealing/corrosion structures as needed. Complete customized equipment solutions can be tailored to customer plant area, wastewater load, treatment targets, and budget-balancing safety, economics, and local adaptation-providing compliant, stable, and highly adaptable equipment structural design support for global environmental projects. This design capability is what transforms a generic Biogas Plant Design into a site-specific solution optimized for local POME Treatment conditions and USR Process performance.
Full-Industry-Chain Integrated Delivery Capability
Center Enamel is the only company globally integrating proprietary enamel frit R&D, self-manufactured tanks, and EPC general contracting-full-process self-control from solution design, equipment production, cross-border logistics, overseas construction, to post-construction O&M-significantly reducing client coordination and time costs. This end-to-end capability ensures that every Biogas Plant Design, USR Process system, and POME Treatment project is delivered with consistent quality, optimized performance, and seamless execution-from initial concept through decades of reliable operation.
Ready to develop your POME Treatment project? Contact us today-our team will respond within 24 hours with a customized Biogas Plant Design featuring USR Process technology.
Frequently Asked Questions
1. What makes USR Process ideal for POME Treatment?
The USR Process tolerates high suspended solids, oil, and fiber without clogging. Its simple structure and flocculent sludge operation suit POME‘s extreme characteristics-delivering stable anaerobic digestion and high biogas yields.
2. How does Biogas Plant Design affect long-term project economics?
Proper design integrates tank corrosion protection, gas-tightness, temperature control, and process sizing-maximizing biogas recovery, minimizing maintenance, and ensuring 5–8 year payback typical of POME projects.
3. Why choose Center Enamel for integrated biogas projects?
Center Enamel combines 30+ years of GFS tank expertise, in-house R&D, USR Process knowledge, and full EPC delivery-30,000+ global projects with proven long-term performance.