How Biogas Plant Project Design and the USR Process Meet Global Wastewater Standards
Global industrial wastewater treatment policies are escalating from "compliance discharge" to mandatory "resource recovery" and "zero liquid discharge." The EU, through its Circular Economy Action Plan, requires member states to increase industrial wastewater reuse rates and extends carbon footprint accounting to the full life cycle of wastewater treatment. China continuously updates and tightens industrial water pollutant discharge standards, with increasingly stringent limits on total nitrogen, total phosphorus, and characteristic pollutants for industries such as chemicals, pharmaceuticals, and printing and dyeing. Some water-scarce regions and highly polluting industries are mandated to adopt zero or near-zero liquid discharge technologies. Germany has established a differentiated pretreatment technical standard system by industry, requiring industrial wastewater to meet specific quality requirements before discharge into municipal wastewater treatment plants, implementing strict source control.
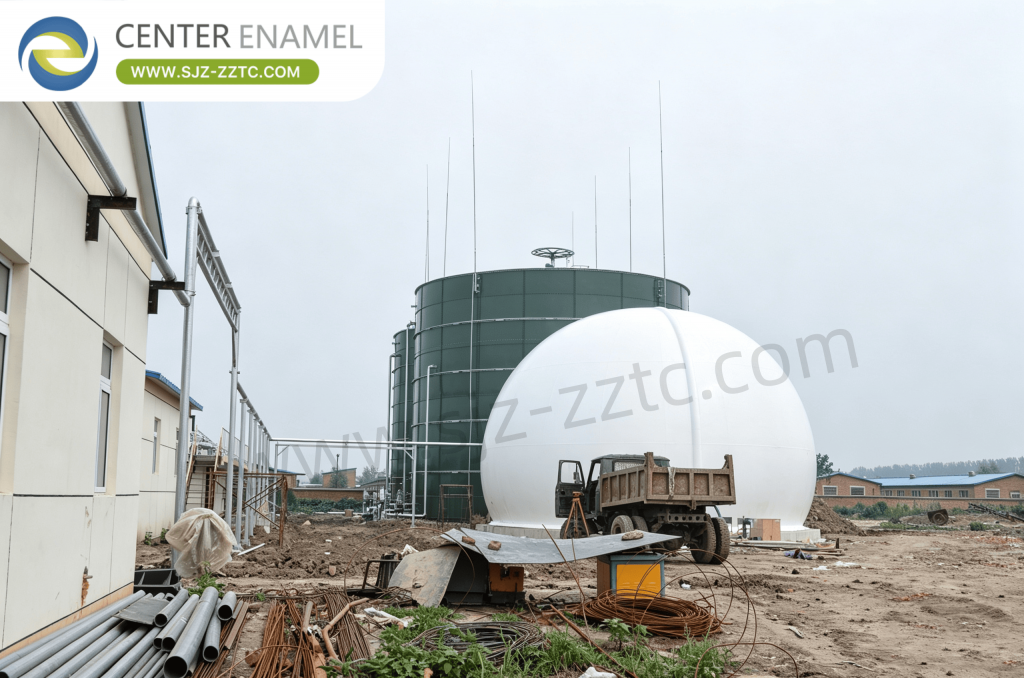
These policy trends directly shape Biogas Plant Project Design priorities-shifting the objective from simple discharge compliance to maximum resource recovery and energy self-sufficiency.
USR Reaction Process for High-Solids Organic Wastewater
High-solids organic wastewater, after simple pretreatment to remove large debris, is uniformly fed into the reactor through the bottom distribution system. The upward flow drives solid substrates and anaerobic sludge to slowly rise and thoroughly mix. In the sealed anaerobic environment, microorganisms sequentially hydrolyze/acidify and then methanogenically ferment, degrading macromolecular organic pollutants and generating biogas and treated water.
Without complex separation structures, gentle hydraulic disturbance prevents clogging. The mixed liquor rises to the upper portion of the reactor where natural gas-liquid-solid separation occurs. Biogas is collected, effluent overflows, and solid sludge and unreacted substrate settle back to the lower reaction zone for continued reaction, with a small amount of aged sludge periodically discharged-continuous stable operation.
The USR Process is often the core biological stage within a complete Biogas Plant Project Design, particularly when influent suspended solids are too high for conventional reactors.
USR Process Reaction Stages and Outputs
| Stage | Process | Output |
| Pretreatment | Removal of large debris | Uniform feed |
| Bottom Distribution | Upflow hydraulic mixing | Solid-sludge contact |
| Hydrolysis and Acidification | Microbial breakdown | Solubilized organics |
| Methanogenesis | Anaerobic fermentation | Biogas and treated water |
| Gas-Liquid-Solid Separation | Natural settling | Biogas collected; effluent overflow; sludge return |
| Sludge Discharge | Periodic aging sludge removal | Continuous stable operation |
Key Water Quality Characteristics of Food Waste
Food waste wastewater presents prominent "four highs"-high COD, high oil and grease, high salinity, high suspended solids-with extremely high pollution load and complex composition. COD typically ranges from 15,000 to 80,000 mg/L, with oil separation wastewater exceeding 100,000 mg/L. Animal and vegetable oil content is extremely high at 5,000 to 20,000 mg/L-oil easily adheres and accumulates on pipe and equipment walls, causing blockages and membrane fouling. High salinity with sodium chloride content of 5,000 to 15,000 mg/L comes from seasonings and salt residues. High suspended solids are rich in food residue particles, bone fragments, and fibrous impurities.
The wastewater is also rich in proteins and amino acids, readily decomposing, emitting odors, and breeding flies. pH is slightly acidic to neutral, BOD/COD approximately 0.4 to 0.5-good biodegradability but oils and salts pose microbial inhibition risks. Water quality varies with collection volume, season, and dietary habits-higher summer volumes with higher oil content.
These characteristics make food waste an ideal candidate for Biogas Plant Project Design that incorporates oil recovery, salinity management, and robust anaerobic digestion.
Food Waste Wastewater Key Parameters
| Parameter | Typical Range | Treatment Challenge |
| COD | 15,000–80,000 mg/L (oil separation >100,000) | Extremely high organic load |
| Oil and Grease | 5,000–20,000 mg/L | Pipe blockage, membrane fouling |
| Salinity (NaCl) | 5,000–15,000 mg/L | Microbial inhibition |
| Suspended Solids | High-food particles, bone fragments, fibers | Clogging risk |
| BOD/COD | 0.4–0.5 | Good biodegradability, but oil and salt inhibit |
| pH | Slightly acidic to neutral | Requires buffering |
| Seasonal Variation | Higher summer volume and oil content | Design flexibility required |
Bangladesh Poultry Farm Manure Resource Recovery Project
This benchmark project targets local poultry farm manure resource recovery with daily treatment of 47 tons. Influent COD, BOD, and SS were as high as 50,000 mg/L, 25,000 mg/L, and 50,000 mg/L. After CSTR + UASB anaerobic treatment, all three parameters were reduced to below 200 mg/L, 100 mg/L, and 100 mg/L-effluent compliant with local environmental discharge standards. The project produces approximately 4,900 m³ biogas daily-each m³ biogas can generate 2 kWh of electricity, with daily power generation of 9,800 kWh-simultaneously achieving pollutant reduction and clean energy recovery. This is a benchmark project for livestock waste recycling in Southeast Asia.
Center Enamel Smart Manufacturing Base Scale
Center Enamel's core intelligent manufacturing base is located in Hebei Province, China, covering a total area of over 150,000 m², with Phase I mature manufacturing facility and Phase II high-end environmental equipment industrial park-dual-base synergy ensures stable production capacity. The base includes dedicated R&D office buildings, proprietary material laboratories, and finished product testing centers, with full-process quality control systems meeting ISO, NSF, CE, and other international standards. The facility operates to green manufacturing standards, certified as a Provincial Green Factory-balancing efficient production with energy conservation and emission reduction.
The company has 6 marketing service centers across China, establishing a nationwide production-sales network ensuring stable global order delivery. The base is adjacent to expressway networks and major logistics hubs, with complete container shipping capabilities-supporting simultaneous large-scale tank projects globally. The base employs over 500 staff, with multiple parallel automated production lines-facility scale and production capacity firmly placing it among the global top tier of GFS tank equipment manufacturers.
This manufacturing scale is what makes complex Biogas Plant Project Design feasible at volume-ensuring tanks, covers, and process components are produced to consistent standards and delivered on schedule.
Full-Industry-Chain Integrated Delivery Capability
Center Enamel is the only company globally integrating proprietary enamel frit R&D, self-manufactured tanks, and EPC general contracting-full-process self-control from solution design, equipment production, cross-border logistics, overseas construction, to post-construction O&M-significantly reducing client coordination and time costs.
This integrated model means the USR Process design, tank fabrication, and on-site installation are managed under one accountable provider-eliminating the interface risks common in multi-vendor projects.
Single and Double Membrane Roof Cover Solution
Single and Double Membrane Roofs are proprietary airtight tank cover systems for anaerobic digestion and biogas storage projects, specifically developed for biogas collection and odor containment, representing a benchmark lightweight sealing solution for fermentation tanks.
The single-layer membrane roof features a simple structure with economical cost, meeting basic biogas containment needs. The double-layer membrane roof consists of inner and outer corrosion-resistant membrane materials, with pressurized air in the interlayer forming rigid support, providing outstanding thermal insulation that reduces biogas condensate formation inside the tank, with enhanced wind and snow load resistance suitable for high-altitude and windy outdoor sites.
The membrane material is specialized aging-resistant and biogas-slurry-corrosion-resistant PVDF membrane, which will not leak or degrade from long-term contact with biogas or hydrogen sulfide. The flexible structure accommodates tank settlement and slight deformation without cracking or gas leakage. The lightweight design eliminates heavy steel support trusses, significantly reducing the load on the tank and foundation, saving construction costs.
The roof integrates biogas outlets, safety pressure relief valves, and access channels, fully enabling closed gas collection for anaerobic fermentation tanks, recovering biogas for power generation and heating while blocking odor diffusion to meet environmental odor control requirements. It is widely used in large-scale livestock biogas projects, municipal sludge anaerobic digestion, and food waste fermentation projects, compatible with large-volume glass-fused-to-steel anaerobic tanks, with fast construction and simple maintenance requiring only periodic membrane seal integrity checks, offering significant overall engineering advantages.
For any Biogas Plant Project Design targeting odor control and methane recovery, the membrane roof is the critical sealing component that makes the system viable.
Single vs Double Membrane Roof Comparison
| Feature | Single-Layer Membrane | Double-Layer Membrane |
| Structure | Simple | Inner and outer membrane with pressurized interlayer |
| Cost | Economical | Higher initial investment |
| Biogas Containment | Basic | Enhanced with thermal insulation |
| Wind and Snow Load | Standard | Enhanced for high-altitude and windy sites |
| Condensate Reduction | Limited | Outstanding |
| Best Application | Basic biogas containment | Large-scale biogas, municipal sludge, food waste |
| Material | PVDF aging and corrosion resistant | PVDF aging and corrosion resistant |
| Maintenance | Periodic seal checks | Periodic seal checks |
Ready to develop a Biogas Plant Project Design built around proven USR Process technology? Contact us today for a customized plan covering design, manufacturing, installation, and long-term O&M support.
With a 150,000 m² manufacturing base and full-industry-chain delivery capability, we turn complex wastewater challenges into compliant, resource-recovery success. Reach out now and let's build your next project together.
FAQ
1. Why is the USR Process important in Biogas Plant Project Design?
The USR Process handles high-suspended-solids wastewater without complex separators or granular sludge cultivation. It prevents clogging, tolerates high impurity loads, and operates stably with flocculent sludge-making it essential for livestock manure, agricultural waste, and food waste streams.
2. How do global policies influence Biogas Plant Project Design?
EU circular economy rules, China's tightening discharge standards, and zero liquid discharge mandates in water-scarce regions all push design toward maximum resource recovery. Biogas plant design must now integrate energy recovery and nutrient reuse, not just pollutant removal.
3. What membrane roof options support biogas collection?
Center Enamel offers single-layer and double-layer membrane roofs. The double-layer version provides thermal insulation, enhanced wind and snow resistance, and outstanding condensate reduction-ideal for high-altitude and windy sites. Both use aging-resistant PVDF membrane compatible with hydrogen sulfide.