
Leading Biogas Project Contractor with CSTR Process for Wastewater Treatment
Global industrial wastewater treatment policies are escalating from "compliance discharge" to mandatory "resource recovery" and "zero liquid discharge." The EU, through its Circular Economy Action Plan, requires member states to increase industrial wastewater reuse rates and extends carbon footprint accounting to the full life cycle of wastewater treatment. China continuously updates and tightens industrial water pollutant discharge standards, with increasingly stringent limits on total nitrogen, total phosphorus, and characteristic pollutants for industries such as chemicals, pharmaceuticals, and printing and dyeing. Some water-scarce regions and highly polluting industries are mandated to adopt zero or near-zero liquid discharge technologies. Germany has established a differentiated pretreatment technical standard system by industry, requiring industrial wastewater to meet specific quality requirements before discharge into municipal wastewater treatment plants, implementing strict source control.
As stringent environmental policies and global carbon neutrality goals reshape industrial compliance worldwide, selecting a reliable engineering partner has become a top priority for facility operators. Collaborating with an experienced Biogas Project Contractor ensures that complex wastewater treatment systems fully comply with rigorous regulatory frameworks. By converting organic waste streams into clean energy assets, industrial facilities successfully navigate tightening emission mandates while achieving long-term environmental sustainability.
CSTR Reaction Process
CSTR operates in continuous feed, continuous reaction, and intermittent/continuous sludge discharge mode, with a concise and coherent process flow. High-solids organic wastewater, after pretreatment to remove large-particle impurities, is fed at a constant rate into the sealed anaerobic reactor via feed pumps. Continuous mechanical stirring maintains uniform mixing throughout the reactor, creating a stable anaerobic environment. Within the reactor, acidogenic bacteria and methanogens decompose macromolecular organic matter in stages, first hydrolyzing and acidifying polysaccharides, proteins, and lipids into volatile fatty acids, then further degrading them into methane and carbon dioxide biogas. Throughout the reaction, no material stratification occurs, pollutants are continuously degraded, treated supernatant overflows from the upper portion of the reactor, aged sludge is periodically discharged from the bottom, and biogas is uniformly collected for resource utilization, maintaining stable sludge concentration and reaction equilibrium for consistent treatment performance.
Achieving high-efficiency organic degradation requires robust biological reaction pathways capable of handling heavy pollutant loads without operational disruption. Implementing a state-of-the-art CSTR Process guarantees uniform mixing, rapid substrate breakdown, and stable methane production within sealed reactor environments. This proven engineering approach effectively eliminates material stratification and optimizes biogas recovery across diverse industrial applications.
Palm Oil Mill Effluent Key Water Quality Characteristics
Prominent "five highs and one low"-high COD, high BOD, high oil and grease, high suspended solids, high temperature, low pH-pollution load far exceeding conventional industrial wastewater, one of the highest concentration wastewater categories in agricultural processing. Very high COD-combined wastewater 45,000-100,000 mg/L, oil separation wastewater peaking above 150,000 mg/L-dozens to hundreds of times higher than municipal wastewater.
High BOD-25,000-65,000 mg/L, BOD/COD 0.5-0.6-excellent biodegradability with very high anaerobic digestion efficiency. High oil and grease-combined 2,000-8,000 mg/L, oil separation above 10,000 mg/L-oil readily adheres and scales on pipe/equipment surfaces, affecting heat transfer and causing blockages. High suspended solids-10,000-20,000 mg/L-primarily fruit pulp residues, fruit shell fibers, colloidal proteins-readily settling and clogging equipment. Moderate total nitrogen-ammonia 500-1,500 mg/L with abundant organic nitrogen but low inorganic nitrogen. High total phosphorus-200-800 mg/L.
Very low pH-raw water pH 4.0-5.0-requires alkali neutralization before biological treatment. High temperature-discharge 60-80°C-requires cooling to 35-38°C before anaerobic digestion. Water quality varies significantly with palm oil mill processing seasons-peak production during fresh fruit bunch harvest season (March-September annually) with full-load operation, wastewater volume and organic concentration at maximum; off-season (October-February) with reduced or halted production-water quality fluctuations require high shock load resistance.
Managing extremely concentrated agro-industrial waste streams like palm oil mill effluent demands comprehensive characterization and specialized treatment strategies. A trusted Biogas Project Contractor designs customized pretreatment and digestion systems tailored to withstand severe temperature, acidity, and organic fluctuations. Consequently, processing plants can successfully mitigate severe environmental hazards while turning complex waste into a valuable renewable power source.
Malaysia Palm Oil Biogas Project
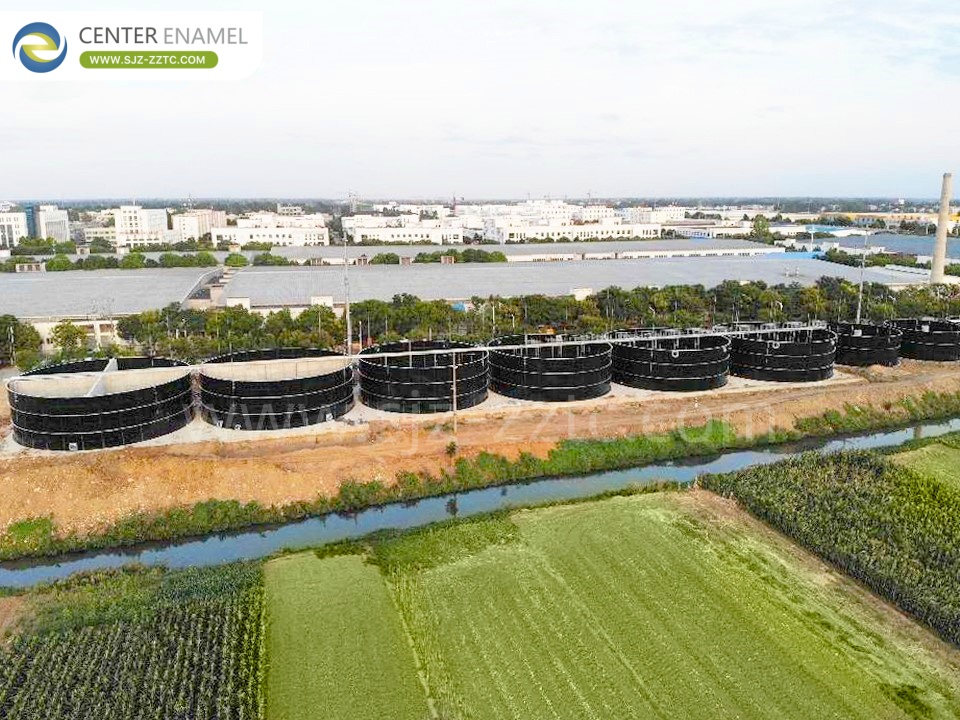
The project uses Center Enamel GFS tanks as the core anaerobic digestion facility with 5 tanks, each with effective volume of 5,400 m³, total effective volume 27,000 m². Influent COD ≥ 60,000 mg/L, BOD ≤ 25,000 mg/L. After anaerobic digestion, effluent COD drops to below 12,000 mg/L, BOD ≤ 5,000 mg/L-overall organic removal efficiency approximately 80%. Single tank daily biogas production 4,400 m³, total project daily biogas 22,000 m³-stable biogas yield of 0.45 m³ per kg COD removed-efficient biogas energy recovery while solving palm oil processing wastewater pollution.
Real-world benchmark projects validate the exceptional performance and economic viability of large-scale industrial anaerobic installations. Deploying an optimized CSTR Process within durable glass-fused-to-steel containment structures ensures maximum organic removal efficiency and stable daily biogas generation. Such successful international implementations demonstrate how advanced environmental engineering transforms regional pollution control into a highly profitable clean energy venture.
Center Enamel's Smart Manufacturing Base Scale
Center Enamel's core intelligent manufacturing base is located in Hebei Province, China, covering a total area of over 150,000 m², with Phase I mature manufacturing facility and Phase II high-end environmental equipment industrial park-dual-base synergy ensures stable production capacity. The base includes dedicated R&D office buildings, proprietary material laboratories, and finished product testing centers, with full-process quality control systems meeting ISO, NSF, CE, and other international standards. The facility operates to green manufacturing standards, certified as a Provincial Green Factory-balancing efficient production with energy conservation and emission reduction. The company has 6 marketing service centers across China, establishing a nationwide production-sales network ensuring stable global order delivery. The base is adjacent to expressway networks and major logistics hubs, with complete container shipping capabilities-supporting simultaneous large-scale tank projects globally. The base employs over 500 staff, with multiple parallel automated production lines-facility scale and production capacity firmly placing it among the global top tier of GFS tank equipment manufacturers.
Delivering high-performance containment systems for international projects requires massive manufacturing infrastructure and rigorous quality control standards. Partnering with a premier Biogas Project Contractor guarantees access to advanced production facilities, certified testing centers, and reliable global supply chains. This exceptional manufacturing capability ensures that every modular tank and reactor component meets the strictest international specifications for long-term operational excellence.
Full-Industry-Chain Integrated Delivery Capability
Center Enamel is the only company globally integrating proprietary enamel frit R&D, self-manufactured tanks, and EPC general contracting-full-process self-control from solution design, equipment production, cross-border logistics, overseas construction, to post-construction O&M-significantly reducing client coordination and time costs.
Minimzing project risks and streamlining cross-border construction schedules depend heavily on unified engineering management and full-industry-chain integration. A capable Biogas Project Contractor manages every phase-from initial design and manufacturing to on-site assembly and long-term maintenance-under a single cohesive framework. This integrated delivery capability eliminates multi-party coordination hurdles and ensures seamless project execution worldwide.
Single and Double Membrane Roof Cover Solution
Single and Double Membrane Roofs are proprietary airtight tank cover systems for anaerobic digestion and biogas storage projects, specifically developed for biogas collection and odor containment, representing a benchmark lightweight sealing solution for fermentation tanks. The single-layer membrane roof features a simple structure with economical cost, meeting basic biogas containment needs. The double-layer membrane roof consists of inner and outer corrosion-resistant membrane materials, with pressurized air in the interlayer forming rigid support, providing outstanding thermal insulation that reduces biogas condensate formation inside the tank, with enhanced wind and snow load resistance suitable for high-altitude and windy outdoor sites.
The membrane material is specialized aging-resistant and biogas-slurry-corrosion-resistant PVDF membrane, which will not leak or degrade from long-term contact with biogas or hydrogen sulfide. The flexible structure accommodates tank settlement and slight deformation without cracking or gas leakage. The lightweight design eliminates heavy steel support trusses, significantly reducing the load on the tank and foundation, saving construction costs.
The roof integrates biogas outlets, safety pressure relief valves, and access channels, fully enabling closed gas collection for anaerobic fermentation tanks, recovering biogas for power generation and heating while blocking odor diffusion to meet environmental odor control requirements. It is widely used in large-scale livestock biogas projects, municipal sludge anaerobic digestion, and food waste fermentation projects, compatible with large-volume glass-fused-to-steel anaerobic tanks, with fast construction and simple maintenance requiring only periodic membrane seal integrity checks, offering significant overall engineering advantages.