
How Can an EPC Contractor Deliver a USR Reactor Solution for Palm Oil Wastewater Treatment Project?
The competitive landscape shows divergence, with leading companies building integrated service capabilities through technical integration and capital operations, and industry concentration gradually increasing. Chinese companies continue to consolidate their advantages in mid-tier equipment exports. International giants target high-end customers and complex industrial wastewater markets, while local players occupy the mid- to low-end and industrial park centralized treatment markets with service responsiveness and cost advantages.
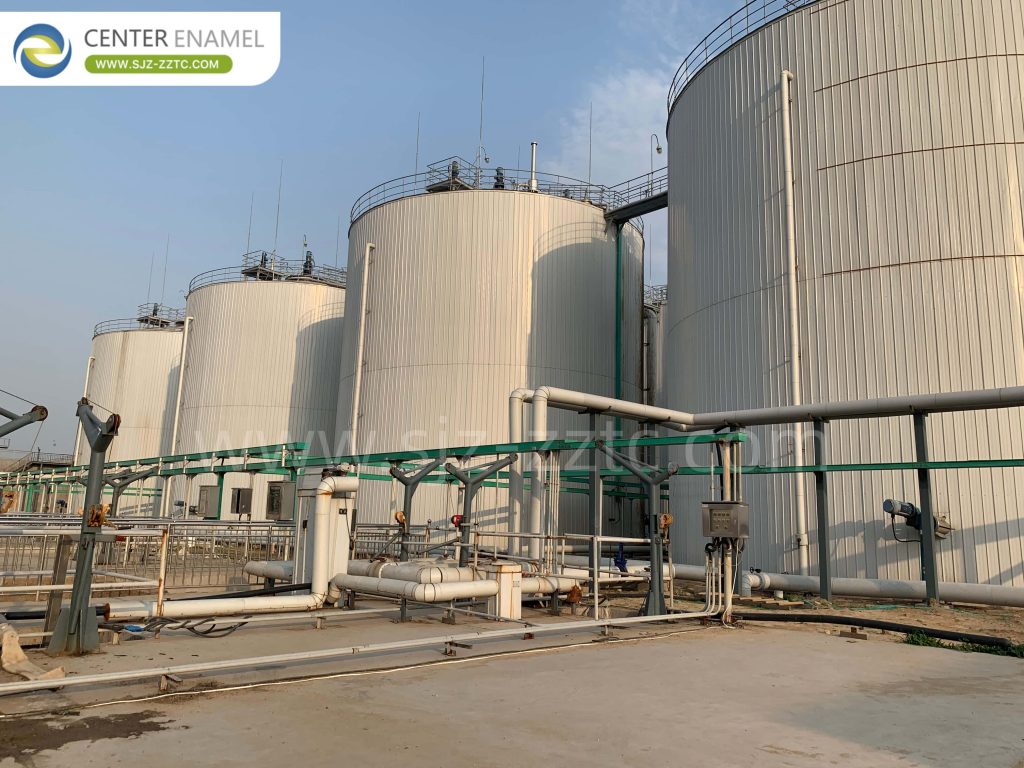
In the anaerobic process segment, UASB, EGSB, and IC anaerobic reactors, with advantages of high loading rates, small footprints, and stable operation, are widely used in high-concentration organic wastewater pretreatment in food processing, pharmaceutical fermentation, alcohol brewing, chemical, and other industries. These reactors use steel tank shells, and their corrosion resistance and gas-tightness directly determine long-term operational stability. The application value of glass-fused-to-steel tanks in such scenarios is increasingly prominent. This market shift toward integrated, long-term operational reliability naturally raises the question of how tank infrastructure performs under the most demanding field conditions-particularly in remote or disaster-prone regions where project success depends on durability as much as process design.
GFS Tanks Engineered for Extreme Climates and Seismic Zones
GFS tanks can undergo customized wind and seismic design based on project site climate and geological conditions, with environmental adaptability far superior to concrete tanks. Concrete tanks are cast-in-place monolithic structures, with seismic and wind resistance entirely dependent on on-site construction quality. In remote areas, typhoon-prone zones, and earthquake belts, construction quality is difficult to control. Under strong earthquakes or typhoons, concrete tanks are prone to cracking and base settlement damage, with subsequent reinforcement costs equivalent to rebuilding.
GFS tanks undergo collection of local seismic intensity, maximum wind pressure, and foundation bearing capacity data before construction, with customized thickened steel panels, stiffening ribs, and anchored base components-all factory-prefabricated to standardized specifications. The bolted panel structure has excellent stress distribution capability, making it less prone to overall fracture under seismic and typhoon impacts, and minor foundation settlement will not cause through-cracking. Structural parameters can be flexibly adjusted for mountainous, coastal typhoon-zone, and high-seismic-zone projects, providing long-term protection against extreme natural climate damage. These structural advantages are especially critical for anaerobic treatment systems, where gas-tightness and dimensional stability directly affect biological performance. It is this very combination of structural resilience and process compatibility that makes GFS tanks the preferred choice for USR Reactor applications in challenging environments.
USR Reactor Supporting Equipment and System Integration
Core equipment is the GFS tank with no complex media or precision three-phase separators, featuring a rugged clog-resistant structure. Bottom large-diameter anti-clogging distribution system suitable for high-solids wastewater, preventing pipe clogging. Supporting equipment includes influent lift pumps, simple pretreatment screens, and equalization tanks for impurity removal and water quality balancing. Simple top gas collection devices and biogas conveying/desulfurization equipment for biogas resource recovery.
Temperature, level, and pH online monitoring equipment. Bottom large-diameter sludge discharge pipes and pumps for rapid removal of high-concentration residual sludge, suitable for high-solids conditions. The complete system has extremely low failure rates, outstanding wear and clog resistance, and is far easier to maintain than conventional anaerobic processes. This rugged, low-maintenance configuration makes the USR Reactor particularly well-suited for the extreme water quality characteristics of palm oil mill effluent-a challenge that demands a fully integrated engineering approach rather than isolated equipment supply.
Standardized Palm Oil Wastewater Treatment Project Solutions
Core treatment uses a mature train of “oil separation/cooling pretreatment + CSTR/USR anaerobic digestion + aerobic treatment + advanced treatment”-perfectly suited for POME‘s high-concentration, high-oil, high-temperature, low-pH characteristics. Pretreatment: Raw POME first enters oil separation tanks/oil separators to remove free and dispersed oil-recovered palm oil can be sold as a resource, significantly reducing organic load. Cooling towers/heat exchangers reduce temperature from 60–80°C to 35–38°C for mesophilic anaerobic digestion. Lime/NaOH addition adjusts pH from 4.0–5.0 to 6.8–7.2 for optimal anaerobic conditions. Screens and sedimentation tanks remove fruit shell fibers, fruit pulp residues, and other large suspended solids to prevent distribution system and pipe clogging.
Main anaerobic treatment: Center Enamel CSTR or USR Reactor with GFS tanks as core reaction equipment, suited to POME’s high-concentration, high-oil, high-suspended-solids conditions. CSTR mechanical mixing addresses oil floating layers, suspended solids sedimentation, and surface crusting-the three major challenges-ensuring thorough material-microbe contact. USR simplifies internal structure with anti-clogging, high-solids tolerance-suited for high-suspended-solids POME. Single GFS anaerobic tank effective volume 3,000–10,000 m³, with multiple tanks configurable for different mill capacities. Anaerobic digestion HRT 20–30 days, COD removal 80–90%, BOD removal 85–92%, with simultaneous large-volume biogas production.
Aerobic treatment: Anaerobic effluent still has COD 3,000–10,000 mg/L-requiring aerobic polishing. A/O, A²/O, or SBR processes further degrade residual organics and remove nitrogen/phosphorus, reducing COD to 200–500 mg/L and BOD to 50–100 mg/L. Advanced treatment: Depending on discharge standards or reuse requirements, BAF, coagulation/sedimentation, sand filtration, or constructed wetlands reduce COD to below 100 mg/L and ammonia to below 10 mg/L for irrigation reuse or surface discharge compliance.
Biogas utilization: POME anaerobic digestion produces exceptionally high biogas yields-8–15 m³ biogas per m³ wastewater-after desulfurization and dehydration, biogas can be used for CHP, meeting 30–50% of mill electricity demand, with waste heat used for digester heating and FFB sterilization preheating-achieving energy self-sufficiency. Delivering this complex, multi-stage treatment train requires far more than equipment supply-it demands the coordinated expertise of a qualified EPC Contractor capable of integrating design, manufacturing, and construction.
Full-Category Complete Product Matrix of Center Enamel
Center Enamel has built a complete product matrix of “core storage tanks + supporting covers + specialty pressure vessels + complete environmental engineering services”-the only company globally to achieve integrated enamel frit R&D, self-manufacturing, and GFS tank application.
① Core: Proprietary GFS Tanks - Using proprietary double-sided hot-rolled double-layer enamel anti-corrosion technology-resistant to strong acids/alkalis, high salinity, and microbial corrosion-modular quick assembly-suitable for all strong-corrosion conditions in wastewater, biogas, and chemical applications.
② Supporting: Fusion Bonded Epoxy Tanks - Produced on China‘s first intelligent standardized production line-primarily for drinking water, fire water, and neutral medium storage.
③ Sealing: Aluminum Dome Covers - Proprietary high-strength aluminum alloy self-supporting structure-meeting international waterproof and load-bearing standards-suitable for tank sealing and biogas collection.
④ Other Tanks: Carbon Steel Tanks, Stainless Steel Tanks, Composting Tanks, Various Non-Standard Pressure Vessels.
⑤ Engineering Services: Environmental EPC General Contracting, Anaerobic Process Section Subcontracting-one-stop coverage across food waste, leachate, municipal wastewater, livestock biogas, petrochemical/metallurgical, and seawater desalination industries-customizable tank volume, corrosion protection grade, and complete process solutions with integrated equipment manufacturing and engineering construction.
This comprehensive capability is precisely what positions Center Enamel as a dependable EPC Contractor for complex projects such as a Palm Oil Wastewater Treatment Project, where multiple technologies must work in seamless harmony.
Center Enamel Marketing Team and Global Project Support
The marketing team brings together environmental industry multi-skilled professionals and multilingual foreign trade specialists, with deep expertise in global biogas, wastewater treatment, and biomass new energy markets-accumulating extensive practical project experience in Southeast Asia, Africa, Europe, and the Americas.
The team is proficient in various countries’ wastewater discharge regulations, biogas subsidy policies, and carbon trading rules-providing one-stop preliminary site survey, solution planning, and investment return analysis consulting services. With multilingual capabilities (English, French, Spanish, Arabic), the team effectively communicates with clients worldwide-precisely matching regional industrial resources, project budgets, and environmental requirements-customizing high-cost-performance GFS tanks and anaerobic reactor solutions based on client production capacity, treatment targets, and gas production expectations.
Leveraging extensive overseas project experience, the team proactively helps clients avoid risks in overseas approvals, equipment import, and construction implementation-building a globally adaptable integrated environmental equipment business service system. This front-end consulting capability, combined with full in-house engineering and manufacturing, allows Center Enamel to function as a true single-point EPC Contractor for international clients seeking a reliable USR Reactor solution.
Aluminum Alloy Trough Deck Roof for Water Storage Applications
Aluminum Alloy Trough Deck Roof is a cost-effective economical tank cover solution for clean water and wastewater storage scenarios, primarily designed for drinking water, production wastewater, and firewater reserve tanks, balancing practicality and cost advantages. The main body is integrally formed from anti-corrosion aluminum alloy plates, paired with aluminum support trusses. Its lightweight design imposes less load on the tank foundation, reducing civil construction investment. A naturally formed dense oxide protective layer on the surface resists rain and mild wastewater corrosion, withstands outdoor sun and rain exposure, and effectively blocks wind, rain, insects, fallen leaves, and odor volatilization, protecting water quality by preventing dust and debris from falling in and causing secondary contamination. The flat roof structure is neat and orderly, allowing installation of maintenance walkways, guardrails, vents, and level monitoring ports on top, facilitating daily inspection and equipment maintenance.
The simple sealing structure enables straightforward installation with short construction timelines, and virtually eliminates the need for anti-corrosion painting maintenance, resulting in extremely low operational costs. It is suitable for various small, medium, and large atmospheric pressure water storage tanks, and has been widely implemented in waterworks clear water tanks, industrial circulating water tanks, park firewater tanks, and domestic wastewater temporary storage facilities. It is highly compatible with water storage applications that do not require biogas collection or high-pressure sealing-complementing the broader GFS tank and USR Reactor portfolio offered by Center Enamel as a full-service EPC Contractor.
Ready to move your project forward? Contact Center Enamel today-our team will respond within 24 hours with a customized USR Reactor and GFS tank proposal for your Palm Oil Wastewater Treatment Project.
Frequently Asked Questions
1. What does an EPC Contractor do for a Palm Oil Wastewater Treatment Project?
An EPC Contractor handles engineering, procurement, and construction-from process design and GFS tank manufacturing to USR Reactor installation, commissioning, and O&M support-delivering a single-point turnkey solution.
2. Why choose a USR Reactor over conventional anaerobic systems?
The USR Reactor tolerates high suspended solids, oil, and fiber without clogging. It eliminates complex three-phase separators, operates stably with flocculent sludge, and suits POME’s extreme characteristics.
3. Can Center Enamel manage overseas project delivery?
Yes. With multilingual teams, certified international construction crews, and 30,000+ global projects, Center Enamel provides end-to-end EPC Contractor services across Southeast Asia, Africa, Europe, and the Americas.