Leading USR Reactor Manufacturer – Advanced Anaerobic Treatment Solutions
In today's industrial landscape, wastewater treatment has become a crucial focus for both environmental and economic reasons. Among the various wastewater treatment methods, the Upflow Sludge Blanket (USR) reactor has gained significant attention due to its ability to efficiently treat high-strength organic wastewater. USR reactors are widely used in industries such as food and beverage production, chemical processing, pharmaceutical manufacturing, and livestock farming. The technology allows for the treatment of wastewater with high organic content, providing an eco-friendly and cost-effective solution.
What is a USR Reactor?
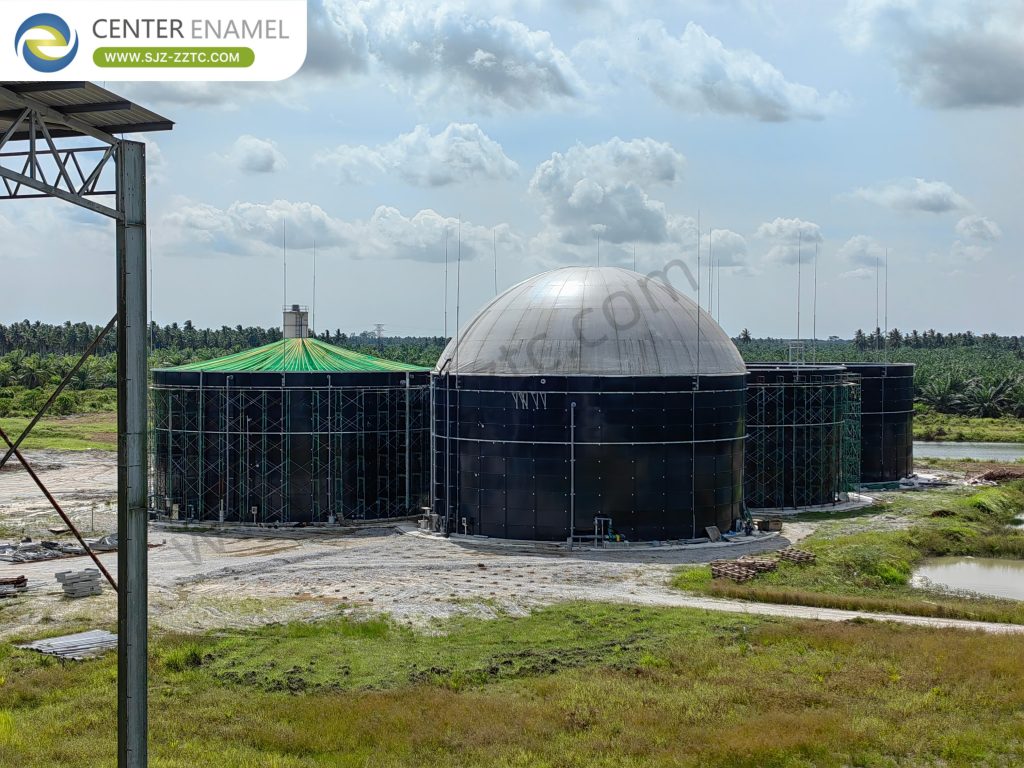
A USR (Upflow Sludge Blanket) reactor is an anaerobic treatment system designed to treat high-strength wastewater. It works by allowing wastewater to flow upwards through a bed of sludge, where anaerobic bacteria break down organic pollutants. The reactor operates in an upflow mode, ensuring that the wastewater interacts with the microbial community for an extended period, allowing for the efficient degradation of contaminants.
The USR reactor is particularly effective for treating wastewater with high chemical oxygen demand (COD), biological oxygen demand (BOD), and total suspended solids (TSS). The process is anaerobic, meaning it does not require oxygen, making it highly energy-efficient compared to aerobic treatment methods. Additionally, the reaction process produces biogas, primarily methane, which can be captured and used as a renewable energy source, further enhancing the sustainability of the process.
Center Enamel - Leading USR Reactor Manufacturers
The market for USR reactors is competitive, with several manufacturers offering advanced solutions tailored to meet specific industrial needs. Below are some of the leading USR reactor manufacturers, renowned for their technological expertise and high-quality products.
Shijiazhuang Zhengzhong Technology Co., Ltd. (Center Enamel)
Shijiazhuang Zhengzhong Technology Co., Ltd. (Center Enamel) is one of the most prominent manufacturers of USR reactors globally. The company specializes in the design and production of advanced wastewater treatment systems, including USR reactors, which are widely used across industries such as food and beverage, pharmaceuticals, aquaculture, livestock farming, and chemical processing.
Center Enamel's USR reactors are designed with cutting-edge technology that ensures optimal treatment efficiency while minimizing operational costs. The company's reactors are built with glass-fused-to-steel (GFS) tanks, offering exceptional durability and corrosion resistance. These reactors are engineered to deliver high COD and BOD removal rates, while the methane produced in the anaerobic process can be recovered as biogas, providing a renewable energy source for industrial operations.
Technological Advancements in USR Reactor Systems
The USR reactor technology has seen several key advancements in recent years, making it even more efficient and sustainable. Some of the key technological innovations include:
1. Energy Recovery and Biogas Utilization
The ability to recover biogas produced during the anaerobic treatment process is one of the most significant advancements in USR reactor technology. The methane produced during the breakdown of organic matter can be captured and used as a renewable energy source. This not only reduces the environmental impact of the treatment process but also helps industries offset their energy consumption, lowering operational costs.
2. Automated Monitoring and Control Systems
Modern USR reactors are equipped with automated control systems that monitor key parameters such as COD, BOD, temperature, and methane production. These systems provide real-time data, allowing operators to adjust the process as needed and ensure that the reactor is operating at peak efficiency. Automated monitoring systems also help with troubleshooting, identifying potential issues before they become major problems.
3. Modular and Scalable Designs
Many USR reactor manufacturers are now offering modular and scalable reactor designs. This allows businesses to install a system that is tailored to their current needs, with the ability to expand the system as wastewater treatment demands grow. Modular designs are also easier to maintain and upgrade, making them a flexible option for industries with evolving treatment requirements.
4. Enhanced Sludge Management
Advanced sludge management systems have been integrated into USR reactors, improving the overall efficiency of the treatment process. These systems help to optimize sludge retention and ensure that the microbial community remains active for efficient pollutant degradation. Enhanced sludge management also reduces the need for frequent maintenance and sludge disposal, contributing to cost savings and environmental sustainability.
Project Overview: USR Reactor Implementation for Livestock Wastewater Treatment
Project Background
Center Enamel successfully designed and supplied a comprehensive wastewater treatment system for a large-scale hoggety (pig farm) in Guangdong Province, China. The project addressed the challenge of treating high-strength livestock wastewater generated from water-submerged manure cleaning operations.
Scope of Work
The project scope included the engineering design, manufacturing, and supply of a multi-stage treatment system tailored to the farm's specific wastewater characteristics. The system was designed to handle the farm's daily wastewater output while meeting local environmental discharge standards.
Technologies Used
The treatment system employs a combined three-stage process:
| Stage | Technology | Function |
| Stage 1 | Pre-process (Screening & Equalization) | Removal of large solids, grit, and flow balancing |
| Stage 2 | USR (Upflow Sludge Blanket) Reactor | Anaerobic digestion of high-strength organic matter; biogas generation |
| Stage 3 | AOAO (Anaerobic-Oxic-Anoxic-Oxic) Process | Biological nitrogen and phosphorus removal; final polishing |
| Project Parameter | Detail |
| Location | Guangdong Province, China |
| Wastewater Source | Manure cleaning by water submerging (pig farm) |
| Treatment Capacity | 300 m³/day |
| Treatment Process | Pre-process + USR + AOAO (3-stage system) |
| Application | Hoggety / Pig Farm Wastewater |
| System Type | Integrated anaerobic + aerobic biological treatment |
Note: Actual effluent quality depends on influent variability and operational conditions. The AOAO post-treatment stage ensures effective nitrogen and phosphorus removal to meet discharge standards.
Client Testimonials
"Center Enamel's integrated USR + AOAO system has provided a reliable solution for our pig farm's wastewater treatment needs. The multi-stage process effectively handles the high organic load from our manure cleaning operations, and the system operates stably with minimal intervention." – Farm Operations Manager, Guangdong Province
"The combination of anaerobic USR pretreatment and aerobic AOAO polishing gives us confidence that we are meeting environmental compliance requirements. The technical support from Center Enamel throughout the project was professional and responsive." – Environmental Compliance Officer, Guangdong Province
Center Enamel's Vision for the Future of USR Reactor Technology
As one of the leading manufacturers of USR reactors globally, Shijiazhuang Zhengzhong Technology Co., Ltd. (Center Enamel) has been committed to advancing wastewater treatment technologies, particularly in the development and application of USR reactors. Center Enamel's USR reactors not only provide efficient wastewater treatment solutions but also focus on continuous technological improvements to meet increasingly stringent environmental regulations and industry demands.
1. Continuous Innovation and Investment in Research and Development
Center Enamel believes that the development of USR reactor technology must align with environmental protection requirements and sustainable development goals. To achieve this, the company continually increases its investment in research and development, optimizing the design of existing USR reactors to improve processing capabilities and energy efficiency. The company plans to drive the future development of USR reactor technology through several key initiatives.
2. Sustainable Development and Environmental Responsibility
Center Enamel has always regarded sustainable development as the core goal of its product research and development. In the design and application of USR reactors, the company not only focuses on treatment performance and economic benefits but also strives to reduce energy consumption and environmental pollution. Going forward, Center Enamel will continue to optimize the environmental performance of its USR reactors to ensure that its products comply with global environmental regulations.
3. Customizable Solutions for Clients
With the continuous expansion of global markets, Center Enamel recognizes that each industry and client has unique needs. To better meet the diverse needs of its clients, Center Enamel will continue to offer customized USR reactor solutions. Whether for the food and beverage industry, pharmaceuticals, aquaculture, livestock farming, chemicals, or other sectors, Center Enamel's USR reactors can be tailored to meet specific wastewater treatment needs.
4. Global Expansion and Market Development
As a global leader in USR reactor manufacturing, Center Enamel continues to strengthen its global strategic presence. The company has not only established a dominant position in the domestic market but is also actively expanding into international markets, providing efficient wastewater treatment solutions to industries worldwide. By establishing branches and partnerships, Center Enamel can better understand the regulatory requirements in different countries and regions, offering products and services that meet local market demands.
Frequently Asked Questions (FAQ)
Q1: What industries benefit most from USR reactor technology?
A: USR reactors are widely used in food and beverage processing, pharmaceutical manufacturing, chemical production, aquaculture, and livestock farming (particularly hog/pig farm wastewater) — industries that generate high-strength organic wastewater with elevated COD, BOD, and TSS levels.
Q2: How does a USR reactor differ from a UASB reactor?
A: While both are anaerobic upflow systems, the USR (Upflow Sludge Blanket) reactor is specifically optimized for wastewater with high suspended solids content, whereas UASB (Upflow Anaerobic Sludge Blanket) reactors are typically better suited for soluble COD effluents with moderate TSS levels. The USR reactor maintains a high-concentration sludge blanket without mechanical stirring, making it more tolerant of solids and shock loads.
Q3: What is the typical COD removal efficiency of a USR reactor?
A: Under optimal operating conditions, USR reactors typically achieve COD removal efficiencies of 75% to 85%. When combined with aerobic post-treatment stages such as AOAO, overall system COD removal can exceed 95%.
Q4: Can the biogas produced be used as an energy source?
A: Yes. The biogas produced during anaerobic digestion is primarily methane (55–65%) and carbon dioxide. It can be captured and used for on-site heating, electricity generation, or as a fuel substitute, significantly reducing operational energy costs and carbon footprint.
Q5: How does the AOAO process complement the USR reactor?
A: The AOAO (Anaerobic-Oxic-Anoxic-Oxic) process is an aerobic biological treatment stage that follows the anaerobic USR reactor. While the USR effectively removes organic matter (COD/BOD), the AOAO stage further removes residual organics, ammonia nitrogen, and phosphorus, ensuring the final effluent meets stringent discharge standards for livestock wastewater.