UASB Wastewater Treatment for Palm Oil Mill Effluent (POME)
Palm oil production is a cornerstone of Southeast Asian economies, yet it generates palm oil mill effluent (POME) —a high-strength wastewater characterized by extreme organic loading, elevated suspended solids, and substantial oil and grease content. POME typically exhibits COD concentrations ranging from 40,000 to 100,000 mg/L, with a pH of 4–5 and discharge temperatures of 40–90°C .
Untreated POME poses severe environmental risks, including aquatic oxygen depletion, soil contamination, and regulatory non-compliance. Among the advanced treatment technologies available, the Upflow Anaerobic Sludge Blanket (UASB) reactor has emerged as an effective and sustainable solution for treating high-strength industrial wastewater such as POME.
What Is a UASB Reactor?
A UASB reactor is an anaerobic digestion system that treats wastewater by facilitating the breakdown of organic matter under oxygen-free conditions. Wastewater flows upward through a dense blanket of granular sludge rich in anaerobic microorganisms. These microorganisms metabolize organic compounds, producing biogas—primarily methane and carbon dioxide—as a byproduct.
The upward flow promotes intimate contact between wastewater and the microbial community, enhancing organic matter degradation and ensuring substantial COD reduction. The modular design of UASB reactors allows for scalability and adaptability to varying wastewater volumes, making them particularly suitable for the fluctuating loads typical of palm oil mills .
Characteristics and Challenges of POME
POME is a byproduct of palm oil extraction and is characterized by:
High organic matter concentration: COD of 40,000–100,000 mg/L
High suspended solids: Fibers and sediment that can cause operational issues
Elevated oil and grease: Can block light and gas exchange in water bodies
Low pH: Typically 4–5, requiring pH adjustment before biological treatment
High temperature: 40–90°C discharge temperature, often requiring cooling for mesophilic treatment
These characteristics make POME particularly challenging to treat using conventional methods. Untreated or inadequately treated POME can lead to severe environmental pollution affecting both terrestrial and aquatic ecosystems.
How UASB Systems Address POME Treatment
Core Operating Principle
In a UASB reactor tailored for POME treatment, wastewater is introduced at the bottom and flows upward through the sludge blanket. As effluent percolates upward, granular sludge captures and degrades organic matter, converting it into biogas. Key operational parameters—including hydraulic retention time (HRT), organic loading rate (OLR), temperature, and pH—are carefully controlled to optimize microbial activity .
Performance Data: UASB and Modified UASB Systems for POME
| Reactor Configuration | Temperature | HRT | OLR | COD Removal | Biogas/Methane Yield | Source |
| UASB-HCPB (thermophilic) | 55°C | 2 days | 27.65 g COD/L·d | 90% COD, 90% BOD | 60% methane content | |
| UASB-HCPB (start-up) | 55°C | — | 28.12 g COD/L·d | 88% COD, 90% BOD | 52% methane content | |
| UASB (mesophilic) | ~35°C | 5 days | 5.8 gVS/L·d | >90% COD | 436–438 mL CH₄/gVS-added | |
| UASB-FF (pilot scale) | Mesophilic | 24 hours | — | 48.7% COD | 80% biohydrogen, 36 L/day | |
| UASB-Filtration-RBC (integrated) | Ambient | 2–6 days | — | 58.71% avg COD, 97.52% O&G | — | |
| UASFF (thermophilic) | 50°C | 1.5 days | — | 94% COD | — | |
| UASB-HCPB + Ultrafiltration | 45°C | 6 days | — | >90% COD | 88% methane content |
The data demonstrates that UASB and its modified configurations consistently achieve 88–94% COD removal under optimized conditions, with biogas methane content ranging from 52% to 88% .
Technical and Environmental Benefits
Enhanced Organic Matter Degradation
The UASB reactor's ability to efficiently degrade high concentrations of organic matter is a significant advantage when treating POME. This results in lower residual COD levels, ensuring treated effluent meets stringent environmental discharge standards. Studies confirm >90% COD removal at HRT of 5 days in continuous UASB operation .
Energy Recovery Through Biogas
One of the notable benefits of UASB technology is the production of biogas during anaerobic digestion. The methane-rich biogas can be harnessed as a renewable energy source, offsetting operational costs and contributing to a circular economy within the palm oil industry. Modified UASB systems have demonstrated biogas production up to 3,400 mL with methane content reaching 88% .
Reduced Sludge Production
Compared to aerobic treatment systems, UASB reactors generate considerably less sludge. This reduction decreases disposal costs and minimizes environmental risks associated with sludge management.
Cost-Effective Operation
Due to its anaerobic nature, the UASB process requires lower energy inputs compared to aerobic systems. The combination of energy recovery and reduced maintenance needs translates into lower overall operational costs.
Environmental Compliance
By effectively reducing organic load and producing stabilized effluent, UASB technology helps palm oil mills achieve compliance with increasingly rigorous environmental regulations, including Indonesia's PROPER rating system and ISPO/RSPO certification requirements .
Project Reference: Sri Lanka Palm Oil Wastewater Treatment Project
Project Overview
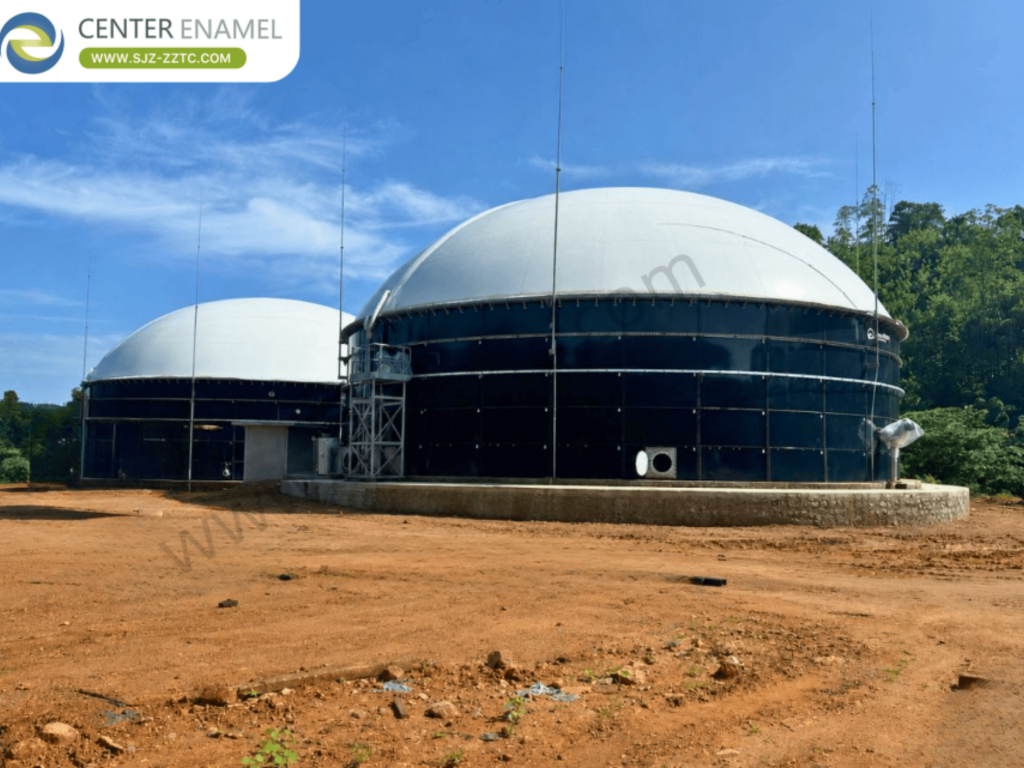
Center Enamel successfully delivered a Palm Oil Wastewater Treatment Project in Sri Lanka in 2026. The project features two large-scale reactor tanks with a daily treatment capacity of 250 tonnes per day, utilizing SBR (Sequencing Batch Reactor) treatment process. The system is designed to treat high-strength palm oil wastewater with exceptional efficiency, reducing COD from 65,600 mg/L to below 400 mg/L, BOD from 7,480 mg/L to below 250 mg/L, and TSS from 14,425 mg/L to compliant discharge levels.
Scope of Work
Design: Customized reactor tank configuration with optimized SBR process
Manufacturing: Two reactors with dimensions of Ø24.46 × 6 m each
Installation: Complete assembly and commissioning on-site
Commissioning: System startup and operational optimization
Technologies Used
Glass-Fused-to-Steel (GFS) Tanks
Center Enamel's GFS tanks serve as high-efficiency reactor vessels. The inert glass-lined interior withstands the corrosive nature of palm oil wastewater, while the robust structure ensures long-term durability in tropical climates.
Project Specifications
| Parameter | Specification |
| Installation Date | 2026 |
| Location | Sri Lanka |
| Daily Treatment Volume | 250 tonnes/day |
| Treatment Process | SBR |
| Reactor Size | Ø24.46 × 6 m, 2 sets |
Wastewater Inlet and Outlet Data
| Parameter | Measured Value (Inlet) |
| COD | 65,600 mg O₂/L |
| BOD | 7,480 mg O₂/L |
| TSS | 14,425 mg/L |
| Parameter | Discharge Standard |
| COD | ≤ 400 mg O₂/L |
| BOD | ≤ 250 mg O₂/L |
| pH | 6.5 – 8.5 |
Project Results and Data
The Sri Lanka project demonstrates the effectiveness of Center Enamel's treatment solutions for high-strength palm oil wastewater:
| Parameter | Inlet Value | Discharge Standard | Removal Efficiency |
| COD | 65,600 mg/L | ≤ 400 mg/L | 99.4% |
| BOD | 7,480 mg/L | ≤ 250 mg/L | 96.7% |
| TSS | 14,425 mg/L | Compliant | >95% |
Client Testimonial
"Center Enamel's SBR treatment system has enabled us to meet stringent discharge standards while handling the high organic load of palm oil wastewater. The two reactor tanks have performed reliably, and the project was completed on schedule. We are highly satisfied with the results."
— Project Manager, Sri Lanka Palm Oil Mill
Frequently Asked Questions (FAQ)
What is POME and why is it difficult to treat?
Palm Oil Mill Effluent (POME) is a high-strength wastewater generated during palm oil extraction. It is difficult to treat due to its extremely high COD (40,000–100,000 mg/L), low pH (4–5), elevated oil and grease content, and high discharge temperature .
How does a UASB reactor treat POME?
A UASB reactor treats POME by flowing wastewater upward through a dense granular sludge blanket containing anaerobic microorganisms. These microbes degrade organic matter, converting it into biogas (methane and carbon dioxide) while reducing COD by 90% or more under optimized conditions .
What COD removal efficiency can UASB achieve for POME?
UASB and modified UASB configurations consistently achieve 88–94% COD removal for POME treatment. At HRT of 2 days and OLR of 27.65 g COD/L·d, 90% COD and BOD removal has been demonstrated .
Can UASB reactors produce biogas from POME?
Yes. UASB reactors produce methane-rich biogas during anaerobic digestion. Biogas methane content ranges from 52% to 88% depending on reactor configuration and operating conditions .
Why are Glass-Fused-to-Steel tanks preferred for POME treatment?
GFS tanks offer superior corrosion resistance against acidic POME (pH 4–5) and hydrogen sulfide. The glass-steel fusion at >820°C creates an inert surface that resists chemical attack, while the modular bolted design enables rapid assembly in remote plantation areas .
Why Choose Center Enamel?
Center Enamel's wastewater treatment systems are at the forefront of this technological advancement. With a commitment to engineering excellence, environmental compliance, and cost efficiency, our solutions are designed to meet the stringent demands of the palm oil industry.
Proprietary enamel formulas: Over 200 patented recipes for superior corrosion resistance
International certifications: ISO 28765, AWWA D103-09, NSF/ANSI 61 compliant
Full-lifecycle EPC service: From design and production to installation and commissioning
Localized design: Adapted to tropical humidity, coastal conditions, and seismic requirements
For palm oil mill operators seeking to enhance wastewater treatment performance and achieve sustainability goals, our treatment solutions represent a compelling choice.
Contact Center Enamel today to learn how our customized solutions can be integrated into your palm oil mill operations.