Why We Use the USR Process to Treat High-Solids Wastewater
High-solids wastewater is the most unforgiving feedstock in anaerobic treatment. Suspended solids, fibrous impurities, and settleable organics clog distribution pipes, smother sludge beds, and shut down conventional reactors that depend on precision internal structures. The USR Process was engineered specifically to solve this problem-trading complexity for ruggedness, and fragility for tolerance.
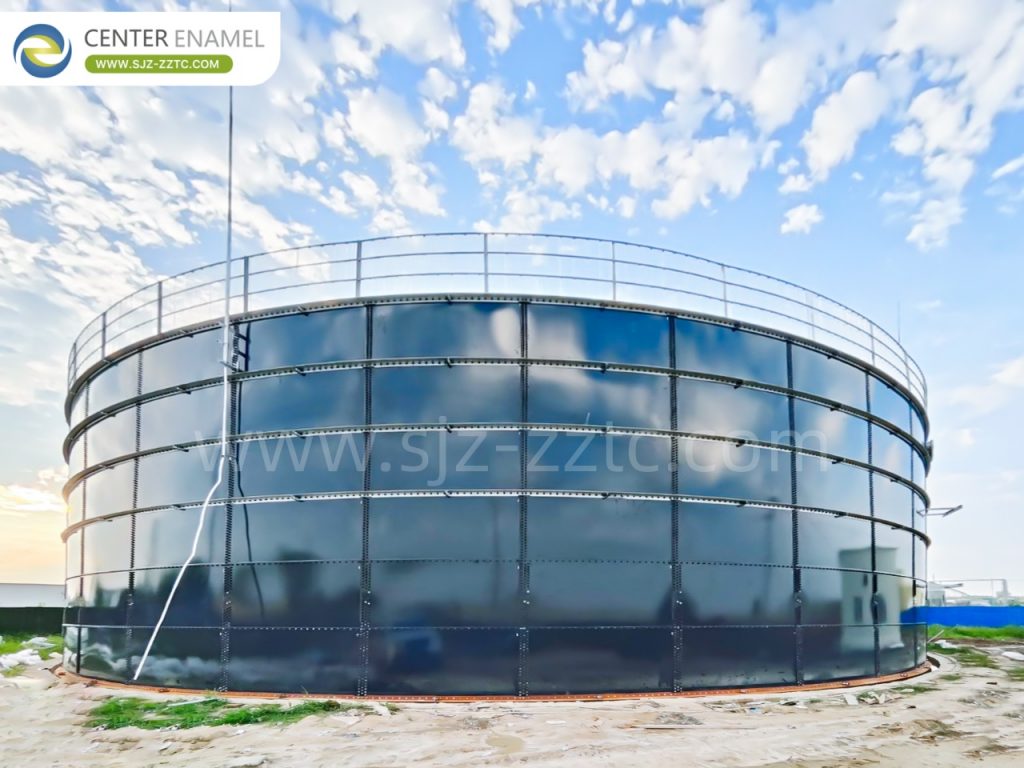
By eliminating precision three-phase separators and narrow-aperture internals, the USR Process handles high-suspended-solids, high-impurity, high-organics wastewater that would incapacitate UASB, EGSB, or IC systems. This article examines the market forces driving demand for such solutions, the specific design logic behind the USR Process, where it applies best, and how the economics of resource recovery make it viable at scale.
Competitive Dynamics Reshaping the Anaerobic Treatment Market
Understanding why the USR Process matters requires context on how the treatment market is evolving. The competitive landscape shows divergence, with leading companies building integrated service capabilities through technical integration and capital operations, and industry concentration gradually increasing. Chinese companies continue to consolidate their advantages in mid-tier equipment exports. International giants target high-end customers and complex industrial wastewater markets, while local players occupy the mid- to low-end and industrial park centralized treatment markets with service responsiveness and cost advantages.
Within the anaerobic process segment specifically, UASB, EGSB, and IC anaerobic reactors-with advantages of high loading rates, small footprints, and stable operation-are widely used in high-concentration organic wastewater pretreatment in food processing, pharmaceutical fermentation, alcohol brewing, chemical, and other industries. These reactors use steel tank shells, and their corrosion resistance and gas-tightness directly determine long-term operational stability. The application value of glass-fused-to-steel tanks in such scenarios is increasingly prominent. Yet these same high-rate reactors share a critical vulnerability: their internal separation and distribution structures are intolerant of high solids. This is precisely the gap the USR Process fills, occupying the segment of the market where feedstock quality is too poor for high-rate reactors but volume is too large to ignore.
Where the USR Process Delivers Its Greatest Value
The USR Process is a dedicated process for agricultural high-solids wastewater, primarily suitable for large-scale livestock manure, livestock soaking water, agricultural straw leachate, and livestock slaughterhouse high-solids wastewater. For high-suspended-solids, high-organics, high-impurity wastewater conditions, it is the core process for rural livestock pollution treatment and agricultural organic waste resource utilization. It is equally suitable for township decentralized wastewater treatment and small to medium-sized agricultural enterprise wastewater treatment.
Beyond livestock applications, the USR Process can serve as the primary process for large livestock base manure resource recovery, combining wastewater treatment with biogas recovery. It is also suitable for various high-solids, easily clogged, difficult-to-treat organic wastewater pretreatment, with superior suitability in agricultural environmental applications compared to other anaerobic processes. The common thread across all these applications is feedstock that would clog, abrade, or overwhelm the internal structures of higher-rate reactors-making the USR Process not merely an alternative, but often the only reliably operable choice.
The Economics of Food Waste Treatment: Costs Offset by Resource Recovery
Process selection is ultimately an economic decision, and here the USR Process paired with GFS Tanks presents a compelling case. O&M costs are moderate to high, but resource recovery benefits are substantial, producing good overall economics. Pretreatment oil removal equipment and three-phase separators require high capital investment, but recovered oil can be sold-biodiesel feedstock oil has good market value, providing core revenue for food waste treatment. Stable biogas from anaerobic digestion can be used for power generation or heating, offsetting energy costs.
The CSTR process has simple equipment with no precision wear parts, keeping maintenance costs low. High-salt, high-oil conditions require premium corrosion protection such as GFS Tanks, with higher initial investment but long service life and low maintenance. Chemical consumption is mainly flocculants and desulfurizers-a moderate expenditure. Oil and salt cause pipe fouling and membrane pollution, requiring periodic cleaning and moderate labor input. Overall, resource recovery revenues from oil sales, biogas energy, and digestate fertilizer generally cover O&M costs, delivering good overall economics. This revenue-offset dynamic is what transforms high-solids wastewater treatment from a cost center into a resource recovery operation.
Case Study: Bangladesh Large-Scale Poultry Farm Manure Resource Recovery Project
The clearest evidence of USR Process and GFS Tanks performance comes from operational data. Center Enamel's Bangladesh project targets local poultry farm manure resource recovery with daily treatment of 47 tons. Influent COD, BOD, and SS reached as high as 50,000 mg/L, 25,000 mg/L, and 50,000 mg/L respectively. After CSTR + UASB anaerobic treatment, all three parameters were reduced to below 200 mg/L, 100 mg/L, and 100 mg/L-effluent fully compliant with local environmental discharge standards. The project produces approximately 4,900 m³ of biogas daily, and each cubic meter of biogas can generate 2 kWh of electricity, yielding daily power generation of 9,800 kWh. This simultaneously achieves pollutant reduction and clean energy recovery, establishing it as a benchmark project for livestock waste recycling in Southeast Asia.
Treatment Performance (Bangladesh Poultry Manure Project)
| Parameter | Influent | Effluent | Standard |
| COD | 50,000 mg/L | < 200 mg/L | Local discharge compliant |
| BOD | 25,000 mg/L | < 100 mg/L | Local discharge compliant |
| SS | 50,000 mg/L | < 100 mg/L | Local discharge compliant |
Energy Recovery Output (Bangladesh Poultry Manure Project)
| Metric | Value |
| Daily treatment capacity | 47 tons |
| Daily biogas production | ~4,900 m³ |
| Electricity per m³ biogas | 2 kWh |
| Daily power generation | 9,800 kWh |
| Outcome | Pollutant reduction + clean energy recovery |
Global Market Presence and Localized Adaptation
Delivering USR Process projects across diverse regions requires both scale and local sensitivity. Center Enamel's global business covers over 100 countries and regions, with 30,000+ successful overseas projects. Products are exported to all major regions including Europe, the Americas, the Middle East, Africa, Southeast Asia, and Latin America, supported by a well-established global localized service network.
Domestically, the company is organized into North, South, Central, East, and Southwest marketing regions, covering environmental, water utility, livestock, and petrochemical customers nationwide. Internationally, the company adopts a "standardized products + localized adaptation" model-adjusting tank corrosion protection, sealing, and pressure standards for different national water quality and environmental regulations. This approach has produced multiple global landmark projects, including large-volume GFS Tanks in Italy, 20 m tower water supply tanks in Colombia, coastal seawater treatment tanks in Costa Rica, and large municipal wastewater aluminum dome projects in Saudi Arabia. The company has established long-term stable strategic partnerships with many Fortune 500 companies-a track record that de-risks USR Process deployment in unfamiliar regulatory and climatic conditions.
Flexible Service Delivery for Overseas and Phased Projects
Project execution capability determines whether a technically sound design actually reaches operation. Center Enamel deploys its own cross-border construction teams alongside a global localized agent network. Modular GFS Tanks assembly enables short construction periods with dismantlable and reusable capability-suitable for overseas short-term projects, phased capacity expansion, and sites where conventional civil construction would be impractical. This delivery model is particularly relevant for USR Process installations in rural or remote agricultural settings, where local construction resources may be limited and project timelines sensitive to seasonal waste generation cycles.
Aluminum Alloy Trough Deck Roof for Water Storage Applications
Not every tank in a treatment facility requires gas-tight sealing, and selecting the appropriate cover controls cost without sacrificing protection. The Aluminum Alloy Trough Deck Roof is a cost-effective economical tank cover solution for clean water and wastewater storage scenarios, primarily designed for drinking water, production wastewater, and firewater reserve tanks, balancing practicality and cost advantages.
The main body is integrally formed from anti-corrosion aluminum alloy plates, paired with aluminum support trusses. Its lightweight design imposes less load on the tank foundation, reducing civil construction investment. A naturally formed dense oxide protective layer on the surface resists rain and mild wastewater corrosion, withstands outdoor sun and rain exposure, and effectively blocks wind, rain, insects, fallen leaves, and odor volatilization-protecting water quality by preventing dust and debris from falling in and causing secondary contamination. The flat roof structure is neat and orderly, allowing installation of maintenance walkways, guardrails, vents, and level monitoring ports on top, facilitating daily inspection and equipment maintenance. The simple sealing structure enables straightforward installation with short construction timelines, and virtually eliminates the need for anti-corrosion painting maintenance, resulting in extremely low operational costs. It is suitable for various small, medium, and large atmospheric pressure water storage tanks, and has been widely implemented in waterworks clear water tanks, industrial circulating water tanks, park firewater tanks, and domestic wastewater temporary storage facilities. It is highly compatible with water storage applications that do not require biogas collection or high-pressure sealing.
Want to know if the USR Process fits your high-solids wastewater profile? Send Center Enamel your water quality data for a feasibility assessment and process recommendation. Our engineers will design a USR-based solution sized to your treatment targets and budget.
Frequently Asked Questions
Q: What makes the USR Process different from UASB or IC reactors?
The USR Process eliminates precision three-phase separators and narrow internals, using a rugged clog-resistant structure with large-diameter distribution. It tolerates high solids, fibers, and impurities that would clog high-rate reactors-ideal for manure and agricultural wastewater.
Q: Which wastewater types suit the USR Process best?
It excels with livestock manure, soaking water, straw leachate, slaughterhouse wastewater, and other high-suspended-solids, high-impurity organics. It also serves as pretreatment for difficult organic streams and suits decentralized rural treatment.
Q: Is the USR Process economical despite high-solids challenges?
Yes. Simple equipment with no precision wear parts keeps maintenance low, while biogas and recovered oil generate revenue. Resource recovery income typically offsets O&M costs, and GFS Tanks protect the investment with 30+ year service life.