USR Bioreactor for Distillery Wastewater Treatment Project
The global distillery industry, a cornerstone of beverage production, faces a major environmental challenge: the management of its wastewater. This effluent, often called distillery spent wash or vinasse, is characterized by an exceptionally high organic load, high acidity, and an elevated temperature. If discharged without proper treatment, it can cause severe water pollution, damage ecosystems, and result in significant regulatory fines. Faced with the urgent need for sustainable and cost-effective solutions, distilleries are increasingly turning to advanced anaerobic digestion technologies, with the Upflow Sludge Reactor (USR) standing out as a premier choice.
As a leading China USR Bioreactor Manufacturer, Shijiazhuang Zhengzhong Technology Co., Ltd (Center Enamel) is at the forefront of this environmental innovation. We specialize in designing and building high-efficiency, robust anaerobic digestion systems that not only purify wastewater but also convert waste into valuable renewable energy. Our comprehensive expertise and state-of-the-art technology make us the ideal partner for any Distillery Wastewater Treatment Project aiming for environmental compliance, energy self-sufficiency, and long-term sustainability.
The Unique Challenges of Distillery Wastewater
Distillery wastewater presents a unique set of characteristics that demand a highly specialized treatment approach. Its key features include:
Extremely High Organic Load: The effluent contains significant amounts of dissolved sugars, alcohols, and other organic matter from the fermentation and distillation process. This results in an exceptionally high organic load, making it a prime candidate for biogas production but also a major pollutant.
High Acidity: The wastewater is typically acidic, which can inhibit the activity of many microorganisms and requires careful management to ensure optimal biological treatment.
Elevated Temperature: The effluent is often discharged at a high temperature, which needs to be precisely controlled for mesophilic or thermophilic digestion.
Complex Composition: Distillery wastewater contains a complex mixture of organic compounds that require a specialized and robust microbial community to break down effectively.
Effectively addressing these challenges requires a solution that is both highly efficient at removing pollutants and capable of handling fluctuations in flow and composition. This is where the USR Bioreactor excels, offering a proven and powerful method to transform this problematic waste stream into a source of clean energy and water.
The Mechanism of the USR Bioreactor
The USR Bioreactor is a next-generation anaerobic treatment system specifically designed to handle high-strength industrial wastewater. Its mechanism is based on the principle of anaerobic digestion, where a dense layer of microbial sludge facilitates the breakdown of organic contaminants in the absence of oxygen.
Within the reactor, wastewater is introduced at the bottom, allowing it to flow upward through a concentrated microbial sludge bed. As the wastewater ascends, the microorganisms within the sludge granules rapidly consume the organic matter, converting complex compounds into simpler molecules and, ultimately, into methane-rich biogas and carbon dioxide. This upflow design allows for a compact footprint, a long retention time for the wastewater, and excellent contact between the pollutants and the active biomass.
The process is self-sustaining and offers several key advantages for a Distillery Wastewater Treatment Project:
High-Efficiency Pollutant Removal: The dense, highly active granular sludge bed provides an ideal environment for the efficient removal of organic pollutants, ensuring the treated effluent meets stringent discharge standards.
Energy Recovery: A significant benefit of the anaerobic process is the production of valuable biogas. This methane-rich gas can be captured and used as a renewable energy source to power the distillery, helping to offset energy costs and reduce reliance on fossil fuels.
Low Operational Costs: Unlike aerobic systems that require continuous aeration, the anaerobic USR Bioreactor operates with minimal energy input. This results in lower operational costs over the long term.
Reduced Sludge Production: The anaerobic process generates significantly less excess sludge compared to traditional aerobic systems, which further reduces waste disposal costs and simplifies post-treatment management.
Operational Stability: The robust nature of the granular sludge bed allows the reactor to handle variations in wastewater flow and organic load, ensuring stable and reliable performance.
Center Enamel: A Premier China USR Bioreactor Manufacturer
As a leading China USR Bioreactor Manufacturer, Center Enamel provides far more than just a containment vessel. We offer a holistic, integrated solution that encompasses the entire lifecycle of a Distillery Wastewater Treatment Project. Our expertise in engineering, process design, manufacturing, and on-site construction ensures a seamless and successful project delivery from start to finish.
The foundation of our superior systems is our proprietary Glass-Fused-to-Steel (GFS) tank technology. These tanks are the ideal choice for any anaerobic digestion project due to their unparalleled durability and structural integrity. The vitrified glass coating is thermally bonded to the steel surface, creating an impermeable, inert barrier that provides maximum protection against the acidic and corrosive components often found in distillery wastewater and the produced biogas. This ensures a long service life with minimal maintenance, leading to the lowest lifetime cost.
Our GFS tanks offer several key advantages:
Unmatched Corrosion Resistance: The inert glass surface provides an excellent barrier against the corrosive nature of the wastewater and biogas, ensuring the long-term integrity of the reactor.
Rapid, Modular Construction: The modular, bolted design of our tanks allows for swift and safe on-site installation, significantly reducing project timelines and labor costs.
Exceptional Gas-Tightness: Precision engineering and advanced sealants guarantee minimal biogas leakage, maximizing recovery for energy use and preventing fugitive methane emissions.
Hygiene and Easy Maintenance: The smooth, inert surface prevents bio-fouling and simplifies cleaning, promoting a healthy microbial environment.
By combining our deep process expertise with our superior containment technology, we ensure that every Distillery Wastewater Treatment Project we undertake is built for maximum efficiency and long-term sustainability.
Our Comprehensive Project Approach
As a premier China USR Bioreactor Manufacturer, our approach to every Distillery Wastewater Treatment Project is methodical and client-focused. We begin with a detailed feasibility study and process design, working closely with clients to understand their specific wastewater characteristics, project objectives, and regulatory requirements. Our highly experienced engineers then develop a customized system design that may include:
Pre-treatment: Crucial for removing suspended solids and adjusting pH to ensure optimal reactor performance.
Anaerobic Digestion: The core USR Bioreactor designed for high-efficiency organic pollutant removal and biogas generation.
Biogas Recovery & Utilization: Integrated systems for capturing, purifying, and utilizing the biogas for on-site energy needs.
Post-treatment: Secondary treatment for polishing the effluent to meet final discharge standards.
Our comprehensive services ensure a single point of responsibility, streamlining the entire process and mitigating risks for our clients. We take pride in our ability to deliver high-quality, reliable, and cost-effective solutions that help businesses meet environmental compliance and achieve energy independence.
Global Project Portfolio: Center Enamel Project Cases
Our extensive project portfolio showcases our unparalleled experience in delivering high-performance solutions for diverse industrial clients, including those with challenging organic waste streams. The following table consolidates our representative project cases across sectors and regions.
Consolidated Project Case Matrix
| Project Type | Location | Tank Quantity | Total Capacity | Application & Results |
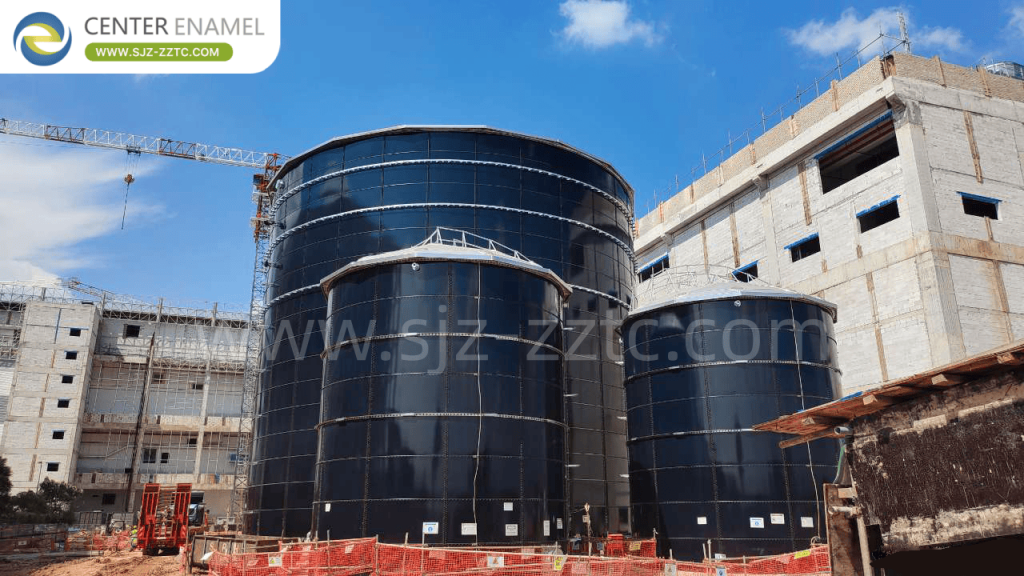
| Distillery Wastewater Treatment | North American Country | 2 tanks | 2,249 m³ | Efficient digestion and biogas production from distillery wastewater |
| Landfill Leachate Treatment | Chinese City | 1 tank | 1,800 m³ | Environmental compliance and operational efficiency |
| Urban and Municipal Sewage | European Country | 1 tank | 1,210 m³ | Tailored solution for a demanding public utility |
| Biogas Engineering | Southeast Asian Country | 1 tank | 1,210 m³ | Energy recovery and sustainable waste management |
| Firefighting Water Storage | Middle Eastern Country | 1 tank | 1,210 m³ | Reliable water storage for a critical safety system |
| Dry Bulk Storage | Latin American Country | 1 tank | 1,800 m³ | Demanding non-liquid storage needs |
Comparative Matrix: USR Bioreactor vs. Conventional Aerobic Treatment
| Evaluation Parameter | Center Enamel USR Bioreactor | Conventional Aerobic Treatment |
| Energy Consumption | Minimal; anaerobic process requires no aeration | High; continuous aeration required |
| Biogas Recovery | Methane-rich biogas captured for energy use | No biogas recovery; energy is consumed |
| Sludge Production | Significantly lower excess sludge | High excess sludge requiring disposal |
| Organic Load Capacity | Handles extremely high organic loads | Limited by oxygen transfer capacity |
| Operational Cost | Low long-term operational cost | High energy and sludge disposal costs |
| Footprint | Compact upflow design | Large footprint required for aeration basins |
| Corrosion Resistance | GFS inert glass surface protects against acidic effluent | Concrete or coated steel vulnerable to acid attack |
Frequently Asked Questions (FAQ)
Q: What makes Center Enamel a leading China USR Bioreactor Manufacturer?
A: Center Enamel combines 30+ years of enameling expertise with a portfolio of projects in over 100 countries. Our GFS tanks are fired at 820–930°C, creating a chemically inert surface that withstands the aggressive acids and corrosive compounds found in distillery wastewater and biogas. We also provide integrated process design covering pre-treatment, anaerobic digestion, biogas recovery, and post-treatment.
Q: What is a USR Bioreactor and how does it treat distillery wastewater?
A: A USR (Upflow Sludge Reactor) Bioreactor is an anaerobic treatment system where wastewater flows upward through a dense microbial sludge bed. Microorganisms consume organic matter, converting it into methane-rich biogas and carbon dioxide. This design provides excellent contact between pollutants and biomass, handles high organic loads, and produces renewable energy as a byproduct.
Q: How does Center Enamel handle the high acidity and temperature of distillery wastewater?
A: Our process design includes pre-treatment for pH adjustment and temperature control to maintain optimal conditions for mesophilic or thermophilic digestion. The GFS tank's inert glass coating provides corrosion resistance against acidic compounds, while insulation and heating systems ensure stable internal temperatures.
Q: What are the economic benefits of a USR Bioreactor for a distillery?
A: The USR Bioreactor reduces operational costs through minimal energy input (no aeration required), generates biogas that can offset fossil fuel costs, and produces significantly less excess sludge than aerobic systems. These factors combine to deliver a lower lifetime cost and faster return on investment.
Q: What certifications do Center Enamel USR Bioreactor tanks carry?
A: Our tanks and equipment meet AWWA D103-09, ISO 28765, NSF ANSI 61, ISO 9001, and CE-EN 1090 standards. These certifications verify structural integrity, manufacturing quality control, and compliance with international engineering requirements.
Engineering the Future of Sustainable Distillery Operations
In a world increasingly focused on sustainability, the USR Bioreactor provides a powerful, proven, and profitable solution for the challenges of distillery wastewater. By choosing a high-efficiency anaerobic digestion system, distilleries can not only achieve regulatory compliance but also transform a waste product into a valuable energy source.
As a leading China USR Bioreactor Manufacturer, Center Enamel stands ready to be your trusted partner. Our integrated approach, combining advanced process knowledge with our superior Glass-Fused-to-Steel (GFS) tank technology, guarantees efficient project delivery, minimized risks, and tailored solutions that meet the specific challenges of your Distillery Wastewater Treatment Project. Let us help you convert your industrial effluent from a burden into a key component of your sustainable future.
Ready to transform your distillery wastewater into renewable energy? Contact Center Enamel today for a free technical consultation and project-specific quote from our engineering team.