USR Bioreactor for Palm Oil Wastewater Treatment Projects
The global palm oil industry, a major player in the food, cosmetic, and biofuel sectors, faces a critical challenge in managing the massive volumes of wastewater it generates. This effluent, known as palm oil mill effluent (POME), is characterized by an exceptionally high organic load, high temperature, and a brownish color. If discharged untreated, it poses a significant environmental threat, contaminating water bodies and soil.
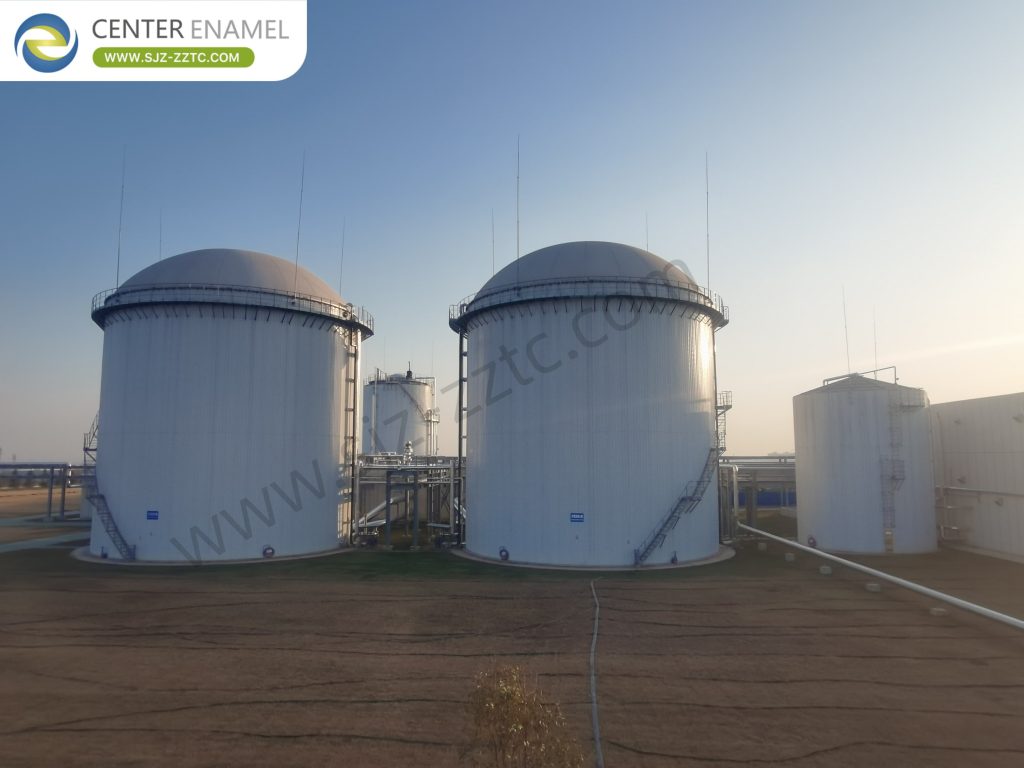
As a leading China USR Bioreactor manufacturer, Center Enamel offers an advanced, high-performance solution for palm oil wastewater treatment projects. Our USR Bioreactor technology is specifically engineered to handle the complex and highly concentrated nature of POME, ensuring environmental compliance, reducing operational costs, and promoting sustainability through valuable energy recovery.
USR Bioreactor for Palm Oil Wastewater Treatment
Understanding the Challenges of Palm Oil Wastewater (POME)
Palm oil mill effluent (POME) is one of the most challenging industrial effluents to treat. Its key characteristics, which present significant treatment hurdles, include:
Extremely High Organic Content: POME has a very high Chemical Oxygen Demand (COD) and Biochemical Oxygen Demand (BOD), with values often exceeding those of typical industrial wastewaters by a significant margin. This high organic load requires a robust system capable of handling very high organic loading rates.
High Temperature: POME is discharged from the milling process at a high temperature (80-90°C), which must be managed to be suitable for biological treatment. While this heat can be a challenge, it also presents an opportunity for heat recovery or direct use in thermophilic anaerobic digestion.
Low pH and Acidic Nature: The wastewater has an acidic pH (typically 4.0-5.0), which can be inhibitory to many microbial populations and requires a system that can handle these conditions.
High Suspended Solids: The presence of large amounts of suspended solids from the milling process can clog traditional systems and inhibit microbial activity.
Variable Composition: The composition and volume of the wastewater can fluctuate based on the specific milling process and fresh fruit bunch quality, requiring a flexible and resilient treatment system.
These factors make effective palm oil wastewater treatment projects a necessity for both environmental protection and sustainable mill management.
The USR Bioreactor: A Superior Anaerobic Technology
The USR Bioreactor (Upflow Sludge Reactor) is an advanced anaerobic digestion system designed for the efficient treatment of high-strength organic wastewater. Unlike conventional digesters, its unique design facilitates superior solid-liquid separation and provides a stable environment for microbial growth. Wastewater enters the reactor from the bottom, flowing upward through a dense granular sludge bed.
This unique design is what makes the USR Bioreactor so effective for palm oil wastewater treatment projects:
High Organic Loading Rate (OLR): The USR Bioreactor can handle extremely high organic loads, which is crucial for the concentrated effluent from palm oil mills. Its efficient sludge retention allows for a high concentration of active biomass, ensuring rapid and effective organic matter degradation.
Superior Treatment Efficiency: The upflow design and the formation of high-density granular sludge ensure intimate and prolonged contact between the wastewater and the microbial community, leading to exceptionally high COD removal rates and stable performance.
Biogas Production and Energy Recovery: A significant advantage of the anaerobic process is the production of methane-rich biogas. This biogas can be captured and used as a renewable energy source to power the mill's operations, offsetting energy costs and reducing reliance on fossil fuels. This contributes to both environmental sustainability and economic viability.
Minimal Sludge Production: The high-rate anaerobic process generates significantly less excess sludge compared to traditional aerobic systems. This reduces sludge handling and disposal costs, which are often a major expense in wastewater management.
Process Stability: The system is highly resilient to variations in wastewater composition and flow, ensuring reliable performance and minimizing the risk of process upsets that can lead to costly downtime.
The Foundation of Our Solution: Glass-Fused-to-Steel Tanks
As a premier China USR Bioreactor manufacturer, Center Enamel ensures the long-term reliability and durability of its bioreactors by using our proprietary Glass-Fused-to-Steel (GFS) tank technology. GFS tanks are the ideal choice for palm oil wastewater treatment projects due to their unparalleled corrosion resistance and structural integrity.
The GFS manufacturing process involves fusing a silicate glass coating to a steel plate at high temperatures. This creates an impermeable, inert barrier that provides maximum protection against the acidic and corrosive components often found in POME. The modular, bolted construction of GFS tanks allows for rapid and safe on-site installation, significantly reducing project timelines and labor costs. This design also provides flexibility for future expansion, allowing mills to easily scale their treatment capacity as their operations grow.
Project Overview
Center Enamel's USR Bioreactor for Palm Oil Wastewater Treatment Project is an engineered anaerobic digestion solution deployed for palm oil mills treating high-strength POME. The project combines a high-rate Upflow Sludge Reactor process with proprietary Glass-Fused-to-Steel containment to deliver stable COD removal, methane-rich biogas recovery, and minimal sludge production. The modular bolted tank design enables rapid on-site installation and future capacity expansion for mills operating in tropical climates.
Scope of Work
Process design and engineering of the USR Bioreactor anaerobic treatment train for POME
Manufacturing of Glass-Fused-to-Steel (GFS) bioreactor tanks with corrosion-resistant enamel coating
Biogas collection and recovery system integration
Modular bolted tank delivery and rapid on-site assembly
Commissioning, performance verification, and operator training
Expansion planning support for future mill capacity growth
Technologies Used
USR Bioreactor (Upflow Sludge Reactor) anaerobic digestion
Glass-Fused-to-Steel (GFS) tank technology with high-temperature fused silicate glass coating
High-density granular sludge bed for superior solid-liquid separation
Biogas capture and methane energy recovery
Modular bolted tank construction for rapid deployment and scalability
Project Results / Data
| Parameter | Result |
| Feedstock | Palm oil mill effluent (POME) with extremely high COD and BOD |
| Influent temperature | 80–90°C discharged from milling process |
| Influent pH | 4.0–5.0 (acidic) |
| Organic loading rate | Extremely high OLR handled by dense granular sludge bed |
| COD removal | Exceptionally high COD removal rates with stable performance |
| Biogas production | Methane-rich biogas captured for renewable energy use in mill operations |
| Sludge production | Significantly less excess sludge versus traditional aerobic systems |
| Process stability | Resilient to fluctuations in wastewater composition and flow |
| Installation | Rapid modular bolted assembly reducing project timelines and labor costs |
| Scalability | Flexible design enabling future treatment capacity expansion |
| Corrosion protection | Inert glass barrier resistant to acidic and corrosive POME components |
Center Enamel Project Cases
| Project | Units / Capacity | Industry | Highlights |
| Muyuan Group Hubei Suizhou Livestock Wastewater Project | 4 units / 10,750 m³ | Livestock wastewater | Expertise in treating large volumes of livestock wastewater |
| Henan Shuanghui Group Wastewater Treatment Project | 3 units / 4,142 m³ | Meat processing | Foundational and reliable water treatment solution for a major meat processing company |
| Coca-Cola (Jiangsu) Beverage Wastewater Treatment Project | 2 units / 3,026 m³ | Beverage | Tailored solution for a demanding public utility |
| Inner Mongolia Dairy Wastewater Treatment Project | 1 unit / 1,162 m³ | Dairy | Reliable solution for the dairy industry |
| Beijing Urban Wastewater Treatment Project | 1 unit / 1,010 m³ | Municipal | Meets rigorous demands of urban water management |
| Caijiaying Gold Mine Wastewater Treatment Project | 2 units / 2,020 m³ | Mining | Expertise in treating complex mining effluents |
The USR Bioreactor is a game-changing technology for palm oil wastewater treatment projects. It offers a superior combination of efficiency, stability, and sustainability that is unmatched by conventional systems. By choosing a solution from Center Enamel, you are investing in a proven technology built with the highest-quality materials and backed by decades of engineering expertise. Our USR bioreactors not only help palm oil mills meet strict environmental regulations but also enable them to operate more efficiently and contribute to a cleaner, greener future.
Frequently Asked Questions (FAQ)
1. What is a USR Bioreactor and why is it used for palm oil wastewater treatment?
A USR Bioreactor (Upflow Sludge Reactor) is an advanced anaerobic digestion system in which wastewater enters from the bottom and flows upward through a dense granular sludge bed. It is ideal for POME because it handles extremely high organic loading rates, achieves high COD removal, produces methane-rich biogas for energy recovery, and generates minimal excess sludge.
2. How does the USR Bioreactor handle the high temperature and low pH of POME?
POME is discharged at 80–90°C with a pH of 4.0–5.0. The USR Bioreactor's stable microbial environment and resilient process design accommodate these conditions, while the high discharge temperature can be leveraged for heat recovery or thermophilic anaerobic digestion. The GFS tank lining provides inert protection against the acidic effluent.
3. Why are Glass-Fused-to-Steel (GFS) tanks used for USR Bioreactors in palm oil projects?
GFS tanks fuse a silicate glass coating to steel at high temperature, creating an impermeable, inert barrier that resists the acidic and corrosive components of POME. The modular bolted construction enables rapid on-site installation, reduces labor costs, and allows mills to expand treatment capacity as operations grow.
4. What energy recovery benefits does the USR Bioreactor provide to palm oil mills?
The anaerobic process produces methane-rich biogas that can be captured and used as a renewable energy source to power mill operations. This offsets energy costs, reduces reliance on fossil fuels, and improves both environmental sustainability and economic viability.
5. How much sludge does the USR Bioreactor produce compared to aerobic systems?
The high-rate anaerobic process generates significantly less excess sludge than traditional aerobic systems, reducing sludge handling and disposal costs — often a major expense in wastewater management.
6. Can the USR Bioreactor handle fluctuations in POME composition and flow?
Yes. The USR Bioreactor is highly resilient to variations in wastewater composition and flow caused by differences in the milling process and fresh fruit bunch quality. This process stability ensures reliable performance and minimizes the risk of costly downtime.
Ready to upgrade your palm oil mill with a high-performance USR Bioreactor? Contact Center Enamel today for a tailored POME treatment assessment and biogas recovery feasibility study.
Our engineers will help you size the right USR Bioreactor and GFS tank configuration for your mill — reach out now to start your project with a proven China USR Bioreactor manufacturer.