USR Bioreactor for Poultry Farm Wastewater Treatment – Sustainable Anaerobic Solutions
The global poultry industry, a vital source of protein, faces the significant challenge of managing wastewater with a high organic load and complex contaminants. The need for advanced, sustainable, and cost-effective treatment solutions is paramount, driven by both strict environmental regulations and the desire for operational efficiency. Shijiazhuang Zhengzhong Technology Co., Ltd (Center Enamel), as a leading China USR Bioreactor Manufacturer, offers a cutting-edge solution with our precision-engineered Upflow Sludge Reactor (USR) systems. Our expertise in anaerobic digestion technology provides poultry farms with a reliable and powerful tool to transform a complex waste stream into a valuable renewable resource, enhancing profitability and environmental stewardship.
The Unique Challenges of Poultry Farm Wastewater
Poultry farm wastewater, generated from cleaning operations, processing, and manure management, is a particularly challenging effluent to treat. Its characteristics include:
High Organic Content: The wastewater has very high concentrations of organic pollutants, leading to a high Chemical Oxygen Demand (COD) and Biochemical Oxygen Demand (BOD).
High Solids: Significant levels of suspended solids, fats, oils, and grease (FOG) can clog and destabilize conventional treatment systems.
High Nitrogen & Ammonia: The presence of high concentrations of nitrogen compounds, particularly ammonia, can be toxic to microorganisms in many biological treatment processes, inhibiting their ability to break down pollutants.
Variable Flow and Composition: The volume and composition of wastewater can fluctuate significantly depending on the farm's daily operations, requiring a treatment system that is robust and adaptable.
These characteristics demand a specialized treatment system that can effectively handle shock loads and high concentrations of pollutants without compromising stability or performance. Conventional aerobic or simple anaerobic systems often struggle to maintain efficiency in such a challenging environment.
Introducing the USR Bioreactor: A High-Performance Solution
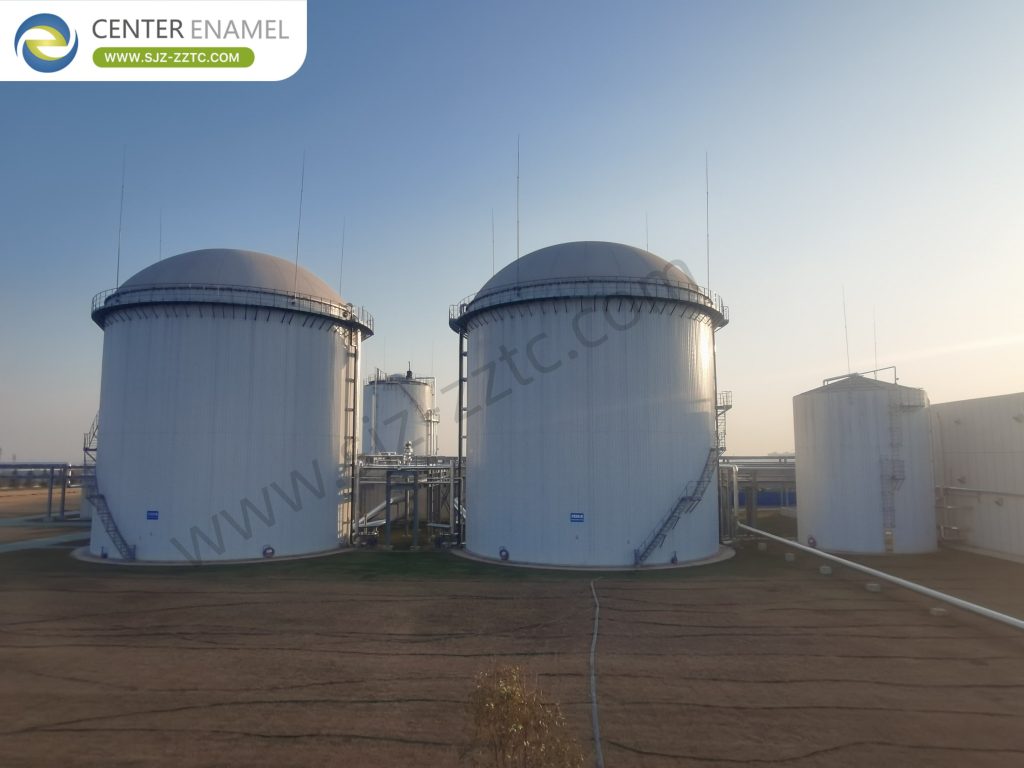
A USR Bioreactor is a high-rate anaerobic digestion system, a more advanced version of the traditional Upflow Anaerobic Sludge Blanket (UASB) reactor. Its operational efficiency stems from its unique design, which is specifically optimized to address the complex challenges posed by poultry farm wastewater.
The core principle of a USR Bioreactor is its upflow mechanism. Wastewater enters the reactor from the bottom and flows upward through a dense, granular bed of anaerobic sludge. As the wastewater passes through this sludge bed, microorganisms in the granules efficiently break down organic pollutants. The system's design facilitates the formation of a robust, highly active microbial community, which is crucial for treating high-strength wastewater.
This process is highly effective due to several key features:
Granular Sludge Formation: The upflow velocity and reactor geometry promote the aggregation of microbial biomass into dense, stable granules. These granules are highly resilient and have a high settling velocity, preventing them from being washed out of the reactor, even at high flow rates.
Internal Circulation & Gas-Lift Effect: As the anaerobic digestion process occurs, the produced biogas bubbles rise to the surface. This gas-lift effect creates a natural internal circulation of the reactor contents, providing gentle but effective mixing. This mechanism ensures optimal contact between the wastewater and the granular sludge, enhancing the degradation process and reducing the need for mechanical mixers.
High Organic Loading Rates: The concentrated, highly active granular sludge allows the USR Bioreactor to handle a very high organic load in a relatively compact footprint. This is a critical advantage for poultry farms with space constraints, as it allows for a more efficient use of land while still achieving a significant treatment capacity.
Exceptional Solids Retention: The bioreactor's design, often incorporating a three-phase separator at the top, ensures a long solids retention time (SRT) while maintaining a short hydraulic retention time (HRT). This means that the valuable microbial biomass is kept within the reactor for an extended period, leading to a highly stable and efficient treatment process.
Advantages of the USR Bioreactor for Poultry Wastewater Treatment
The application of a USR Bioreactor to a Poultry Farm Wastewater Treatment Project offers several compelling advantages that directly address the industry's challenges and enhance overall sustainability.
Effective Ammonia and Nitrogen Management: While anaerobic digestion alone does not remove all nitrogen, the USR Bioreactor's ability to handle high organic loads and fluctuating conditions provides a stable foundation for subsequent treatment stages, such as nutrient removal. By effectively removing COD and BOD in the primary anaerobic stage, it significantly reduces the load on downstream aerobic or anoxic processes, leading to a more efficient and cost-effective overall system.
Biogas Recovery & Energy Generation: A major benefit of anaerobic digestion is the generation of methane-rich biogas. This renewable energy source can be captured and utilized to power on-site operations, such as heating for farm facilities or electricity generation through a Combined Heat and Power (CHP) unit. This turns a waste stream into a valuable revenue source, offsetting energy costs and enhancing the farm's financial sustainability.
Reduced Sludge Production: The anaerobic process produces significantly less excess sludge compared to aerobic methods, which simplifies sludge handling and reduces associated disposal costs. The remaining digestate is a stable, nutrient-rich substance that can be safely used as a bio-fertilizer.
Minimal Odor & Environmental Impact: By containing the anaerobic process within a sealed bioreactor, the system effectively controls odors, which is a major concern for poultry farms. The high treatment efficiency also reduces the risk of environmental pollution and ensures compliance with discharge regulations.
Project Case Studies
Our expertise in implementing tailored solutions for complex environmental challenges is demonstrated through a diverse portfolio of successful projects across various industries and regions.
| Project | Location | Application | Scope | Capacity |
| Poultry Farm Wastewater Treatment | Southeast Asia | Poultry farm wastewater | 1 USR bioreactor | 1,200 m³ |
| Livestock Wastewater Treatment | South America | High-strength livestock wastewater | 4 reactors | 10,750 m³ total |
| Biogas Engineering Project | Eastern Europe | Agricultural biogas production | 2 tanks | 2,249 m³ total |
| Food Processing Wastewater | Middle East | Food processing facility | 1 tank | 1,800 m³ |
| Municipal Sewage Project | China (City) | Municipal water infrastructure | 1 tank | 1,023 m³ |
| Firefighting Water Storage | Europe | Firefighting water storage | 1 tank | 1,210 m³ |
The Center Enamel Difference: As a Leading China USR Bioreactor Manufacturer
As a leading China USR Bioreactor Manufacturer, Center Enamel provides more than just a piece of equipment; we offer a comprehensive, engineered solution. Our expertise lies in designing, manufacturing, and installing high-performance anaerobic digestion systems that are tailored to the unique demands of each project.
Our commitment to quality is evident in our proprietary tank technology. For our USR Bioreactors, we use our premium Glass-Fused-to-Steel (GFS) tanks. This technology combines the strength of steel with the unparalleled corrosion resistance of a glass coating, providing an inert, impermeable barrier that can withstand the harsh and often acidic conditions of wastewater for decades. The smooth, non-porous surface prevents bacterial adhesion and minimizes maintenance. We also provide Fusion Bonded Epoxy tanks and other durable tank solutions, ensuring that every component is built to last.
Our services extend from initial feasibility studies and design to manufacturing, installation, commissioning, and long-term support. We work closely with our clients to analyze their specific wastewater characteristics and design a system that is not only effective but also highly profitable.
Cultivating Sustainability and Profitability
For poultry farm owners and operators, investing in a USR Bioreactor is a strategic move towards a more sustainable and profitable future. This advanced technology not only ensures compliance with environmental regulations but also creates new revenue streams through biogas and bio-fertilizer production.
As a trusted China USR Bioreactor Manufacturer, Center Enamel is dedicated to providing cutting-edge technology, superior product quality, and unparalleled customer support. We are your ideal partner in transforming poultry farm waste into a valuable resource, protecting the environment, and securing a greener, more sustainable future for the agricultural sector.
Frequently Asked Questions (FAQ)
Q1: What is the difference between a USR bioreactor and a UASB reactor?
A: While both are anaerobic upflow systems, a USR (Upflow Sludge Reactor) bioreactor is a more advanced version specifically optimized for wastewater with high suspended solids content, such as poultry farm effluent. The USR reactor maintains a high-concentration sludge blanket without mechanical stirring and features a three-phase separator for exceptional solids retention, making it more tolerant of solids, FOG, and shock loads compared to conventional UASB reactors.
Q2: What is the typical biogas yield from treating poultry farm wastewater in a USR bioreactor?
A: The biogas yield typically ranges from 0.35 to 0.45 m³ per kilogram of COD removed, with methane content between 55% and 65%. For a medium-scale poultry farm processing 300 m³/day of wastewater with a COD of 10,000 mg/L, this translates to approximately 1,000 – 1,200 m³ of biogas per day, which can generate significant energy savings or revenue.
Q3: How does a USR bioreactor handle the high ammonia levels in poultry wastewater?
A: While anaerobic digestion alone does not remove ammonia, the USR bioreactor creates a stable and robust microbial environment that is highly tolerant to ammonia concentrations typical of poultry wastewater (up to 2,000 mg/L). By effectively removing the organic fraction (COD/BOD) in the anaerobic stage, it significantly reduces the organic load on downstream aerobic or anoxic nutrient removal stages, making the overall treatment system more efficient and cost-effective.
Q4: What is the typical lifespan of Center Enamel's glass-fused-to-steel USR bioreactor tanks?
A: Center Enamel's glass-fused-to-steel (GFS) tanks are engineered for long-term durability with a typical lifespan exceeding 30 years. The glass coating is fired at over 800°C, creating a chemically inert and impermeable barrier that provides exceptional resistance to corrosion, abrasion, and harsh wastewater conditions. The smooth, non-porous surface also minimizes bacterial adhesion and reduces maintenance requirements.
Q5: Can a USR bioreactor system be expanded if my poultry farm grows?
A: Yes. Center Enamel offers modular and scalable USR bioreactor designs that allow for future expansion. Our engineering team works with clients to design systems that match current capacity while incorporating flexibility for additional reactors or tank capacity as the farm's wastewater treatment needs grow. This approach protects your investment and ensures the system can evolve with your operations.