What Are the Main Steps in a Biomass Plant?
The main steps in a biomass plant are receiving and storage → pre-treatment (size reduction, drying) → combustion or gasification → heat recovery (boiler/steam) → power generation (turbine/generator) → emissions control → ash handling. In a combined heat and power (CHP) configuration, recovered heat is also exported, lifting total efficiency to 80–90% with 35–45% electrical.
What a Biomass Plant Is
A biomass plant converts solid organic matter—wood, ag residue, palm kernel shell, bagasse—into heat and power. Unlike biogas (wet anaerobic route), biomass is a solid, thermal conversion pathway, so the front end is all about preparing and burning the fuel.
Step 1 – Receiving and Storage
Fuel arrives by truck or conveyor and is stored under cover to control moisture. Reliable, dry, uniform feed is the foundation; poor storage (wet piles, rot) erodes the whole plant’s efficiency downstream.
Step 2 – Pre-Treatment
Biomass is chipped, shredded, or pelletized to a uniform size, and dried toward <10–15% moisture for efficient combustion. Pre-treatment sets the fuel calorific value and feed rate the boiler can use.
Step 3 – Combustion or Gasification
Most plants combust biomass in a grate or fluidized-bed boiler at 800–1000°C, releasing heat. Gasification (partial oxidation, ~700–1000°C) instead makes syngas for engines or turbines—less common but useful for certain residues. Combustion is the utility-scale default.
| Step | Key equipment | Output |
| Receiving/storage | silos, covered yard | conditioned fuel |
| Pre-treatment | chipper, dryer | uniform, dry fuel |
| Combustion | grate/fluidized boiler | hot flue gas |
| Heat recovery | boiler, economizer | steam |
| Power | steam turbine + generator | electricity |
| Emissions | ESP/baghouse, FGD, DeNOx | clean stack |
| Ash | bottom/fly handling | by-product |
Step 4 – Heat Recovery
A boiler turns combustion heat into high-pressure steam; an economizer pre-heats feedwater to squeeze more out. This steam is the plant’s working fluid for power and/or heat export.
Step 5 – Power Generation
Steam drives a turbine-generator for electricity. In CHP, steam extracted at lower pressure delivers process heat or district heating, raising total efficiency to 80–90% (35–45% electrical). Standalone power plants sacrifice the heat and sit lower on total efficiency.
Step 6 – Emissions Control
Flue gas passes an ESP or baghouse (particulates), often FGD (sulfur) and DeNOx (nitrogen), plus careful control of dioxins from certain wastes. Emissions permits dictate the train; biomass is cleaner than coal but not emission-free.
Step 7 – Ash Handling
Bottom ash (coarse, from the grate) and fly ash (fine, from the flue) are collected separately. Both are managed as by-products—see the ash-utilization article—not simply landfill.
Technical Considerations
Fuel moisture and uniformity dominate everything; a 10-point moisture swing can cut efficiency several percent. Boiler fouling from alkali in some biomass (straw, palm) needs design care. CHP only pays if a heat off-take exists nearby.
How to Lay Out a Plant
Match boiler type to fuel (grate for woody, fluidized bed for variable residue), secure a year-round dry fuel supply, and design CHP only with a confirmed heat customer. Size storage for seasonal delivery gaps.
Project Case Study
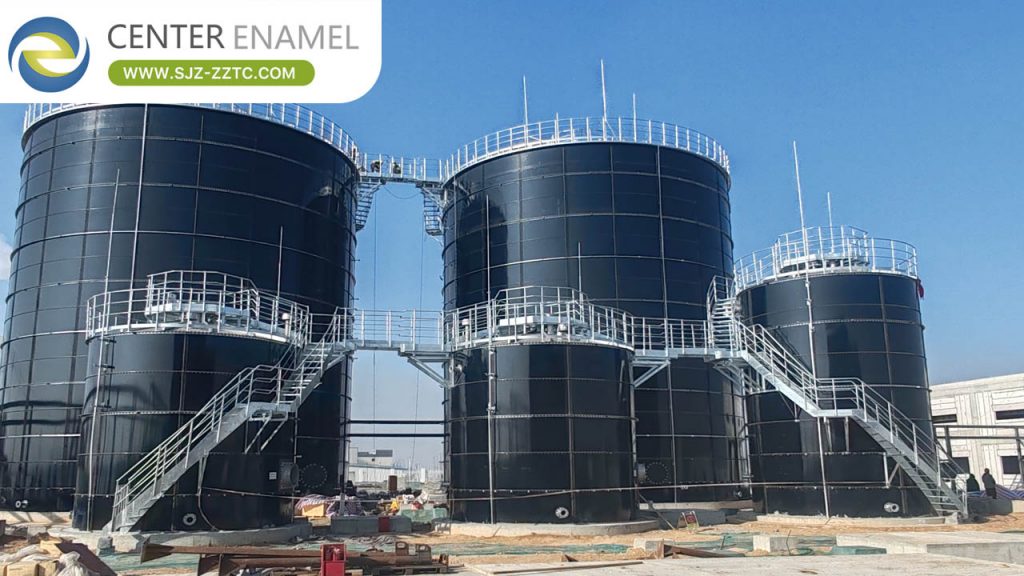
Sri Lanka Palm Oil Wastewater Treatment Project. While an anaerobic (SBR) plant for palm oil mill effluent, it reflects the same biomass/palm sector where solids and fibers are combusted for energy. Center Enamel supplied bolted reactor tanks (Ø24.46 × 6 m, 2 sets) treating 250 tonnes/day of POME, showing tank systems serving palm-mill energy and effluent duty in humid, tropical conditions.
| Project | Sri Lanka Palm Oil Wastewater Treatment |
| Location | Sri Lanka |
| Industry | Palm oil / Agro-industry |
| Application | POME treatment, energy-adjacent |
| Product | SBR bolted reactor tanks |
| Capacity | 250 T/D POME |
| Quantity | 2 Ø 24.46 × 6 m reactors |
| Material | Glass-Fused-to-Steel (GFS) |
| Standards | ISO 28765, AWWA D103 |
| Status | Delivered reference project |
About Center Enamel
Center Enamel brings quality control and standards discipline to biomass and agro-industrial plants: its bolted GFS, epoxy, stainless, and carbon-steel tanks meet ISO 9001 manufacture with ISO 28765 / AWWA D103 (tanks), CE/EN 1090 (structural), and NSF/ANSI 61 / WRAS / FM options for potable-adjacent or fire-duty tanks. For biomass projects the company supplies process water, effluent, and ash-handling storage tanks built to survive humid, corrosive, high-cycling duty, with installation support drawn from dozens of international reference projects.
Advantages and Limitations
Biomass plants give firm, dispatchable renewable power and useful heat (CHP), and can use residues that biogas cannot. Limits: fuel logistics and moisture dominate cost, emissions control is required, and CHP value depends on a heat off-take.
Comparison: Combustion vs Gasification
| Path | Temp | Output | Maturity |
| Combustion | 800–1000°C | steam → power/heat | mainstream |
| Gasification | 700–1000°C | syngas → engine/turbine | niche |
A biomass plant runs receiving → pre-treatment → combustion/gasification → heat recovery → power → emissions control → ash handling. CHP recovers heat to reach 80–90% total efficiency (35–45% electrical); fuel moisture and a real heat off-take decide whether the numbers work.
Frequently Asked Questions (FAQ)
Q1: What are the main steps in a biomass plant?
A: Receiving/storage, pre-treatment (size + dry), combustion or gasification, heat recovery (boiler/steam), power (turbine), emissions control, and ash handling.
Q2: How is energy recovered?
A: A boiler makes steam from combustion heat; a turbine-generator makes electricity, and CHP exports steam heat for 80–90% total efficiency.
Q3: Is combustion or gasification used?
A: Combustion is the mainstream route (grate or fluidized bed); gasification makes syngas and suits specific residues but is less common.
Q4: What about emissions?
A: ESP/baghouse for particulates, plus FGD (sulfur) and DeNOx (nitrogen) as permits require; biomass is cleaner than coal but still regulated.
Q5: What efficiency can I expect?
A: Electrical 35–45% in CHP; total (with heat export) 80–90%; standalone power plants are lower on total efficiency.
Q6: What is the biggest cost driver?
A: Fuel moisture and consistent supply—drying and logistics often decide the project’s economics more than the boiler itself.
Tell us your biomass type, moisture, and whether a heat off-take exists. We will advise tank and storage specifications (process water, effluent, ash) and confirm standards and delivery for your plant.