
Experienced Biogas Project Contractor Delivering USR Process for High-Solids Industrial Wastewater Treatment
The core challenges of industrial wastewater treatment center on the "three highs"-high difficulty, high cost, and high energy consumption. Wastewater from new energy, chemical, and pharmaceutical industries is complex in composition with numerous characteristic pollutants, and traditional treatment processes are difficult to remove effectively. Chinese companies have significant price advantages in the mid-to low-end equipment segment. The industry also faces continuous technological upgrade pressure from increasingly stringent emission standards, as well as new requirements for digitalization and low-carbon transformation on operational refinement management capabilities.
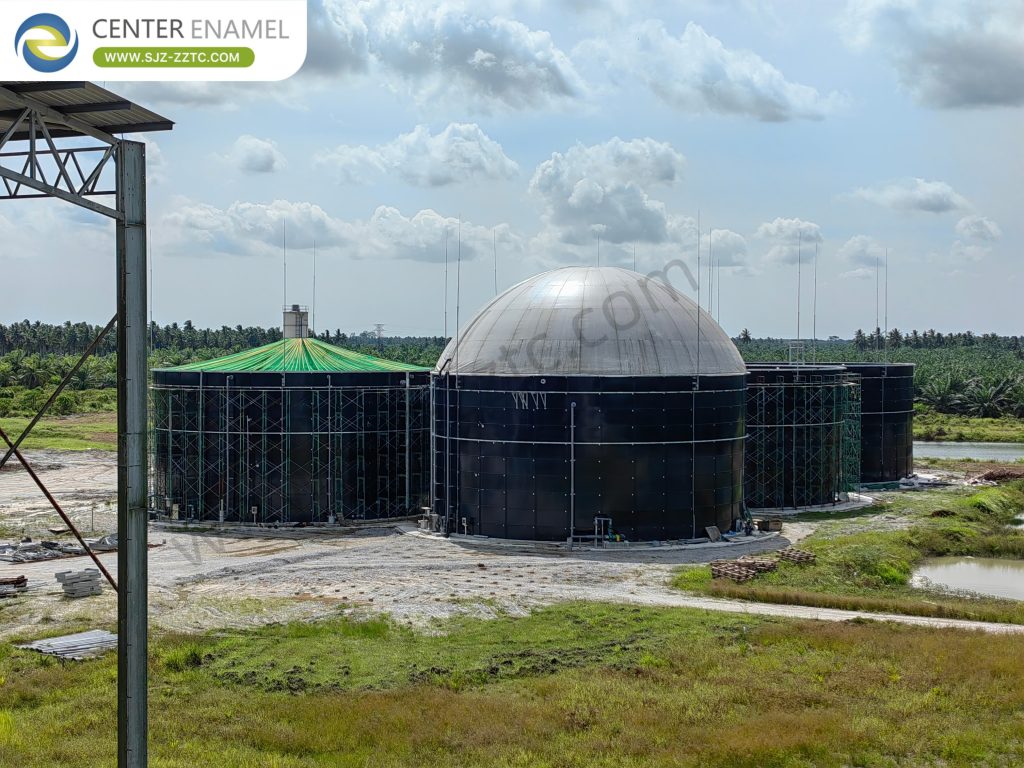
These pressures are especially acute in agricultural and agro-industrial sectors, where high-strength organic wastewater demands treatment trains that are simultaneously robust, economical, and capable of energy recovery. Meeting this triple requirement is precisely the role of a specialized Biogas Project Contractor-one that can integrate process design, durable containment, and long-term operational support into a single accountable delivery. The USR Process has become a core technology in this context, particularly for streams that defeat conventional anaerobic systems.
USR Process Definition: Engineered for High-Solids, Clog-Prone Wastewater
USR, or Upflow Solids Reactor, is an upflow anaerobic process modified for high-suspended-solids, high-solids organic wastewater, specifically designed to solve problems of clogging, sludge washout, and uneven reaction common in traditional anaerobic processes for high-solids wastewater. The process eliminates complex three-phase separators, simplifies internal structure, and relies on upflow hydraulics to promote thorough mixing of solid materials and anaerobic sludge. No strict granular sludge formation conditions are required-flocculent sludge can operate stably. The key feature is high solids tolerance and impurity resistance, with very high influent suspended solids tolerance. It is a dedicated high-efficiency anaerobic process for livestock manure, agricultural organic waste, and high-solids livestock wastewater, specifically developed for agricultural and environmental applications.
This design philosophy-simplicity, robustness, and tolerance for harsh conditions-is what allows the USR Process to function reliably where conventional high-rate reactors would fail. It is also why the process has become a preferred choice for any Biogas Project Contractor serving agricultural and agro-industrial clients. The same characteristics make it directly applicable to palm oil mill effluent, where oil, fiber, and colloidal solids present comparable treatment challenges.
Palm Oil Mill Effluent Wastewater Sources: Understanding the Feedstock Challenge
Palm oil mill effluent (POME) originates from the entire processing chain of fresh fruit bunches (FFB) in palm oil milling-the highest pollution load and largest volume high-concentration organic industrial wastewater in tropical agricultural processing. Palm oil mills typically process 30-120 tons of FFB daily, generating approximately 0.5-1.0 m³ of wastewater per ton of FFB processed-single mills discharging hundreds to thousands of cubic meters daily, representing a core environmental challenge for the palm oil industry. Wastewater comes from three main sources:
(1) Sterilization: FFB enter sterilization vessels for high-temperature steaming to deactivate lipase and prevent free fatty acid increase-producing sterilization condensate, the largest volume source at 80-90°C, rich in soluble sugars, amino acids, organic acids, COD 15,000-30,000 mg/L;
(2) Clarification: Pressed crude oil undergoes centrifugal separation and gravity settling to remove water and impurities-producing large volumes of oily wastewater with extremely high oil content and suspended solids, COD 50,000-80,000 mg/L, the highest organic load source;
(3) Kernel recovery: Palm kernels are separated by hydrocyclones and washed for recovery-producing sandy wash water with high suspended solids but relatively lower organic concentration. Auxiliary discharges include CIP cleaning, floor wash, boiler blowdown, and cooling tower water. POME is acidic (pH 4.0-5.0), high-temperature (60-80°C), brown colloidal, rich in oils, suspended solids, colloidal proteins, and soluble sugars-a typical high-concentration, high-oil, high-suspended-solids organic industrial wastewater.
Understanding these characteristics is essential for any Biogas Project Contractor designing an effective Industrial Wastewater Treatment system for palm oil mills. It is precisely this complexity that makes durable, corrosion-resistant GFS tanks indispensable for POME containment and anaerobic digestion-and it is the reason the USR Process has proven so effective in this application.
30+ Years of Development: From Tank Manufacturer to Comprehensive EPC Service Provider
Center Enamel has been deeply engaged in the environmental bolted storage equipment field for over 30 years. Starting with proprietary enamel anti-corrosion material technology, the company has gradually completed the full-industry-chain upgrade from a single tank manufacturer to a comprehensive environmental EPC service provider. Throughout its 30+ year history, the company has been recognized as a National High-Tech Enterprise, National Specialized and Sophisticated "Little Giant," Manufacturing Single Champion, and Provincial Green Factory. It has successfully delivered over 30,000 environmental projects globally, establishing itself as a leading enterprise in the global GFS tank storage industry. The company has fully integrated the entire chain from enamel frit R&D, intelligent environmental equipment manufacturing, to EPC project contracting-every business breakthrough has been achieved through proprietary core anti-corrosion technology.
This evolutionary path is what distinguishes Center Enamel from equipment-only suppliers and allows the company to operate as a full-scope Biogas Project Contractor. Delivering complete Industrial Wastewater Treatment systems-not isolated tanks or reactors-requires exactly this combination of material science, manufacturing capability, and project execution experience. It also explains why the USR Process can be deployed with confidence across such a wide range of geographies and feedstocks.
Professional Construction Team Manpower Reserve
Center Enamel has established its own domestic and international certified construction teams, with regular practical training on GFS tank installation and overseas construction standards for various countries. Domestically, regional construction teams cover multiple zones, capable of simultaneously deploying multiple teams for large tank farm projects. Internationally, cross-border professional installation teams are equipped to various country construction standards-sufficient manpower reserves ensure uninterrupted construction delivery for remote African sites, high-standard European/American facilities, and other projects.
This construction capacity is a critical differentiator for any Biogas Project Contractor working across multiple regions simultaneously. Whether the project is a USR Process installation in Southeast Asia or a large-scale Industrial Wastewater Treatment facility in Africa, the ability to deploy trained, standards-compliant crews directly determines whether delivery schedules are met.
R&D Team: The Technical Backbone Behind Every Project
Center Enamel has built a full-chain professional team covering R&D, design, marketing, installation, and after-sales. The R&D team is led by national-level materials technology experts, specializing in enamel frit and tank anti-corrosion core technologies. External senior environmental engineering and mechanical structure engineers are retained to strengthen R&D capabilities, focusing on anti-corrosion coating formulations, specialty corrosion-resistant tanks, and anaerobic supporting integrated equipment-continuously breaking through industry technological barriers.
The team operates through proprietary laboratories with external university research collaboration-conducting year-round new material and new process durability pilot testing and long-term corrosion simulation testing. Specialized enamel formulations are iteratively developed for extreme conditions such as high-salinity wastewater, strong acid/alkali POME, and high-organic livestock manure-providing core technical support for the company's annual new invention and utility patents-building a proprietary material technology barrier.
This R&D depth is what separates Center Enamel from ordinary suppliers and allows the company to function as a true Biogas Project Contractor-not merely fabricating GFS tanks, but engineering complete Industrial Wastewater Treatment solutions backed by proprietary material science. It is also what ensures the USR Process performs reliably under the most aggressive real-world conditions.
Innovative Material Technology: 30+ Year Corrosion Resistance for Global Applications
Center Enamel has independently developed over 200 anti-corrosion enamel formulations, with proprietary double-sided double-layer enameling technology-GFS tank anti-corrosion service life exceeds 30 years-far surpassing concrete and ordinary equipment-suitable for global high-corrosion wastewater and biogas fermentation conditions.
Ready to move your project forward? Contact Center Enamel today for expert guidance and a solution built around your specific requirements.
FAQ
What makes the USR Process suitable for Industrial Wastewater Treatment applications?
The USR Process tolerates high suspended solids, resists clogging, requires no granular sludge formation, and starts up quickly. It handles high-oil, high-fiber, high-temperature streams that defeat conventional anaerobic reactors.
Why choose Center Enamel as a Biogas Project Contractor?
We provide integrated design, GFS tank manufacturing, USR/CSTR process delivery, installation, commissioning, and operator training-with 30,000+ projects across 100+ countries and CE, NSF, WRAS, ISO9001, and ASME certifications.
How does Center Enamel support long-term project performance?
Our 24/7 after-sales team provides remote diagnostics, process parameter adjustment, and on-site inspection, with continuous data feedback that improves future USR Process designs.